Heavy-Duty & Multi-Level Pallet Racking Systems
Certified by CE, ISO 9001, ISO 14001, and TUV. Manufactured using high-tensile structural cold-rolled steel designed for maximum volumetric utilization and heavy payload safety.
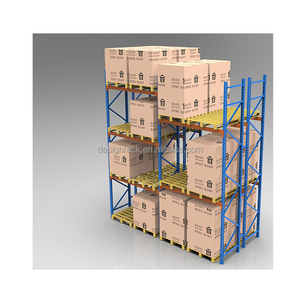
Factory Price Industrial Warehouse Heavy Duty Storage Tray Rack System Pallet Rack Store Shelf
Heavy-duty steel construction with adjustable beam levels, optimized for high load-bearing capacity and warehouse shelf store stability.
Send an Inquiry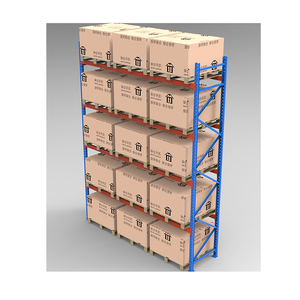
Warehouse Racking Heavy Duty Rack System Stack Warehouse Storage Steel Pallet Racks for Sale
Modular stack steel racking system engineered for industrial pallet handling, offering flexible vertical expansion and durable powder-coated finishing.
Send an Inquiry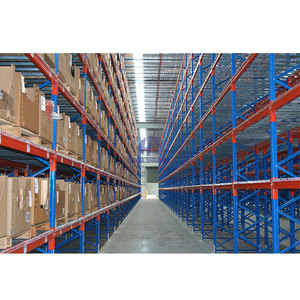
High Performance Heavy Duty Logistics Shelves Stocking Warehouse Storage Rack Pallet Rack for Heavy-Duty Reticulated Shelf
Specialized logistics stocking shelves featuring reticulated wire decking for enhanced fire safety, airflow, and concentrated load safety.
Send an Inquiry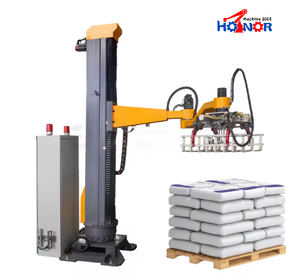
Low Cost 10-50kg Bag Type Pallet Stacker Robot Palletizing Carton Robot Column Palletizing Machine
Automated palletizing robot designed for automated bag and carton stacking directly onto multi-level pallet storage infrastructure.
Send an Inquiry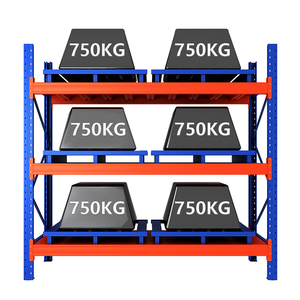
High Load Capacity Heavy Duty VNA Pallet Racks for Warehouse Storage Steel/Metal for Use with Forklift Trucks Save Space
Very Narrow Aisle (VNA) system maximizing vertical storage height while narrowing aisle width to dramatically elevate storage density.
Send an Inquiry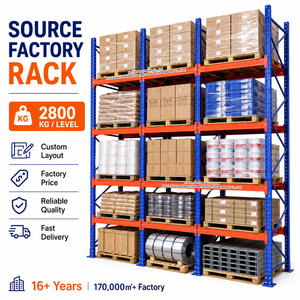
2800KG 5 Levels High Bay Industrial Pallet Racking Heavy Duty Warehouse Rack System
High-bay industrial frame certified for 2800KG capacity per level across 5 multi-tier tiers, ideal for intensive distribution hubs.
Send an Inquiry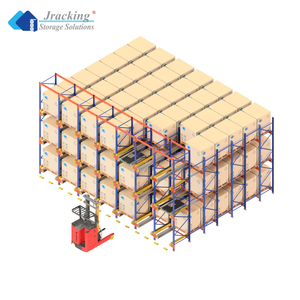
Jracking Automatic Warehouse System Factory Direct Sale High Intelligent Automated Pallet Runner Four Way Radio Shuttle Rack
Intelligent 4-way radio shuttle rack integration providing ultra-high density deep-lane storage with full automation software control.
Send an Inquiry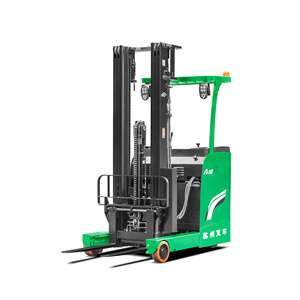
1.5 Ton 2 Ton 2.5 Ton Electric Reach Truck 3m 4m 5m 6m 7m 8m 9m 10m Mast For Narrow Aisle Warehouse Storage
Precision electric reach truck engineered specifically for seamlessly servicing multi-level VNA and high-bay pallet racking structures.
Send an InquiryTechnical Whitepaper: Multi-Level Pallet Racking Systems & Factory OEM Manufacturing
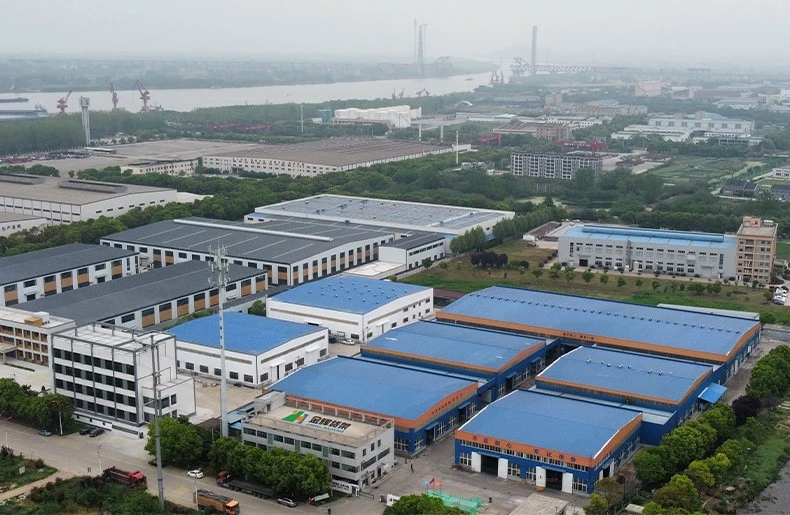
Modern global logistics and supply chain infrastructures demand aggressive vertical cubic spatial utilization without compromising structural integrity, operational safety, or stock rotation velocity. As leading multi-level pallet racking manufacturers operating from a state-of-the-art 40,000 m² manufacturing plant in Nanjing, China, Remprack Storage Solutions Co., Ltd. (established in 2006) provides industrial engineering buyers with certified, structurally validated, high-density storage platforms built according to international standards (EN 15512:2019, FEM 10.2.02, RMI, and ISO 9001).
Multi-level pallet racking—encompassing multi-tier rack-supported mezzanines, high-bay selective pallet systems, teardrop structural frames, Very Narrow Aisle (VNA) systems, and automated 4-way shuttle integration—represents the strategic apex of modern warehouse physical infrastructure engineering.
Precision Cold-Roll Forming & Structural Integrity
Our manufacturing facility utilizes continuous automated cold-roll forming lines designed to process premium structural steel (Q235B, Q355B structural grades). Upright columns feature multi-fold ribbed cross-sections engineered to optimize section modulus, moment of inertia, and buckling resistance under heavy vertical loads up to 28,000 kg per bay.
Every structural component undergoes automated robotic welding, pre-treatment shot blasting, and high-durability electro-static epoxy powder coating (70–90 microns thick), guaranteeing corrosion resistance in ambient, humid, or sub-zero cold storage operations.
Engineering Metrics of Multi-Level & High-Bay Pallet Racks
When selecting a trusted factory and manufacturer for high-bay multi-level rack platforms, structural deflection ratios, dynamic live load distribution, frame stability, and seismic resistance represent non-negotiable procurement criteria.
Structural Steel Integrity
Fabricated using high-tensile cold-rolled steel profiles with multi-point interlocking beam connectors for maximum torsional rigidity and sway protection.
International Compliance
Fully compliant with EN 15512 structural design, CE marking standards, TUV performance verifications, and ISO 14001 environmental management systems.
Custom Engineering & Drawing
Full 2D/3D CAD and BIM modeling provided by experienced structural engineers to ensure optimal layout, aisle clearance, and safety buffer zones.
Detailed Comparative Matrix: Industrial Racking Systems
Understanding the balance between storage density, pallet selectivity, capital expenditure, and operational throughput is vital for warehouse optimization. The technical table below outlines the operational attributes of leading multi-tier rack architectures.
| Racking Architecture Type | Volumetric Storage Density | Pallet Selectivity Ratio | Stock Rotation Method | Forklift / Equipment Requirement | Optimal Industry Application |
|---|---|---|---|---|---|
| Multi-Level Rack Mezzanine | Extreme (200% - 300%) | 100% Direct Access | FIFO / LIFO Flexible | Hand Trucks, Conveyors, Lifts | E-commerce, Auto Parts, Spare Parts Picking |
| Selective Pallet Racking | Standard Baseline (100%) | 100% Direct Access | FIFO (First-In, First-Out) | Standard Counterbalance / Reach | General Logistics, FMCG Distribution |
| Very Narrow Aisle (VNA) | High (+45% vs Selective) | 100% Direct Access | FIFO (First-In, First-Out) | VNA Man-Up / Wire-Guided Reach | High-Bay Distribution Centers, Pharmaceuticals |
| 4-Way Radio Shuttle System | Maximum High-Density (+80%) | Per Lane / Channel Access | Automated FIFO or LIFO | Automated Shuttle + Standard Lift | Cold Storage, Food & Beverage Batch Control |
| Drive-In / Drive-Through | Very High (+60% Density) | Low (Block Stacking) | LIFO (Last-In, First-Out) | Standard Forklift (Enters Rack) | Homogeneous High-Volume SKUs, Seasonal |
Global Sourcing Trends & Industrial Evolution (2025–2030)
The global industrial storage equipment landscape is transitioning rapidly toward semi-automated and fully automated multi-level infrastructures. Strategic procurement directors and logistics system integrators should prepare for four fundamental procurement trends:
1. Hybrid Automated Multi-Tier Storage Systems
Modern distribution hubs are increasingly pairing multi-level rack platforms with automated vertical lift modules (VLMs), autonomous mobile robots (AMRs), and overhead parcel conveyor tracks. This hybrid approach enables high-velocity piece picking on upper walk-way tiers while reserving lower levels for heavy pallet storage and cross-docking operations.
2. Structural Health Monitoring & Sensor Integration
As multi-level racking reaches structural heights of 15 to 30 meters, real-time telemetry monitoring is becoming standard. Wireless strain gauge sensors and impact detection nodes embedded into critical upright posts provide instant alerts regarding forklift collisions or localized beam overload events, ensuring structural resilience and compliance with OSHA / EN safety protocols.
3. Advanced Cold-Formed High-Strength Steels
The steel racking industry is rapidly moving toward micro-alloyed, high-yield steel profiles (such as Q355B and Q420B). These materials allow manufacturers to produce thinner gauge upright columns and box beams that offer equal or higher load capacities compared to traditional hot-rolled sections. This reduction in physical steel weight yields significant cost savings in raw materials and ocean freight shipping expenses.
4. Hot-Dip Galvanizing for Extreme Cold-Chain Environments
With global cold-chain logistics expanding rapidly for pharmaceutical and frozen food products, multi-level rack platforms are requiring specialized anti-corrosion treatments. Hot-dip galvanizing (conforming to ISO 1461) provides total metallurgical bonding, preventing rust degradation in ambient temperatures down to -30°C.
Why Remprack is the Trusted Factory Partner for Global B2B Buyers
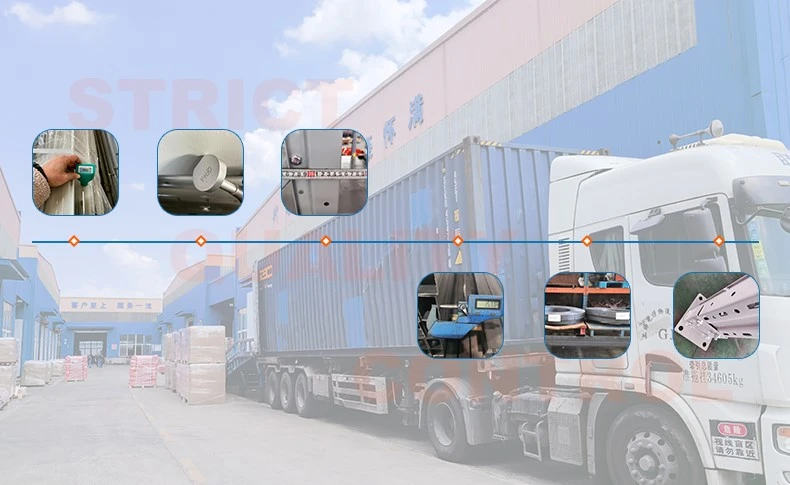
Selecting the right China-based OEM/ODM racking manufacturer requires rigorous supplier verification. Remprack Storage Solutions Co., Ltd. combines technical R&D expertise with robust production capacities designed to mitigate risk for international procurement managers:
- Proven Export Experience: Successfully completed over 2,000 multi-level and heavy-duty storage projects across 85+ countries throughout North America, Europe, Southeast Asia, the Middle East, and Latin America.
- Integrated Manufacturing Control: In-house processing ranging from raw steel coil slitting and automated roll forming to robotic welding, automated powder coating lines, and rigorous dimensional inspection.
- Structural Engineering Guarantees: Every custom multi-level pallet rack system is accompanied by comprehensive engineering calculations, 3D installation drawings, floor slab load distribution analyses, and a 10-year structural warranty.
- OEM & ODM Customization: Custom upright profiles, step beam dimensions, special color matching (RAL spectrum), and brand labeling tailored for international distributors and storage integrators.
Frequently Asked Questions (FAQ) for Enterprise Buyers
What specific technical data is required to design a custom multi-level pallet racking layout?
- Architectural CAD floor plan showing warehouse dimensions, clear building height under trusses/sprinklers, and column grid locations.
- Pallet data: Dimensions (W x D x H including goods), tare weight, and maximum unit load weight (kg).
- Forklift specifications: Maximum lift height, turning radius, and aisle width requirement.
- Operational parameters: Daily throughput, number of SKUs, and local seismic zone requirements.
How do multi-tier rack mezzanine floors comply with fire safety and sprinkler regulations?
What international quality certifications does Remprack hold?
What is the lead time for factory production and container shipment?
Do you provide on-site installation support for overseas projects?
How does a 4-Way Radio Shuttle system compare in cost to a multi-level selective rack?
Transform Your Warehouse Spatial Efficiency Today
Contact our structural engineering team for a free technical consultation, custom CAD layout drawing, and competitive factory-direct quote within 24 hours.