Featured Custom Racking & Automated Systems
Explore high-density heavy-duty rack engineering manufactured directly in China under ISO 9001, CE, and TUV quality compliance.
Executive Report: Sourcing Custom Pallet Racking from China
A structural engineering analysis for global procurement teams, supply chain directors, and warehouse automation integrators.
Structural Engineering Integrity & Steel Standard Selection
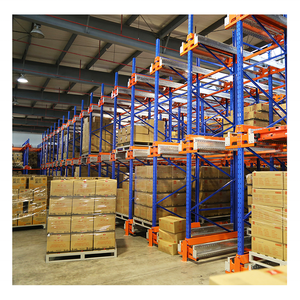
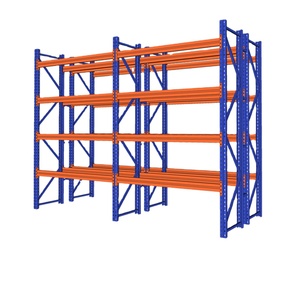
When procurement managers evaluate custom pallet racking system factories in China, technical evaluation must extend far beyond basic dimensions and cost-per-kilo. Structural reliability under full static dynamic loading hinges on raw steel metallurgy. Leading Chinese original equipment manufacturers (OEMs) utilize certified cold-rolled high-tensile structural steel grades such as Q235B (yield strength ≥ 235 MPa) and Q355B / SS50 (yield strength ≥ 355 MPa), fully compliant with international design standards including FEM 10.2.02 (European Federation of Materials Handling), RMI (Rack Manufacturers Institute), and ANSI MH16.1.
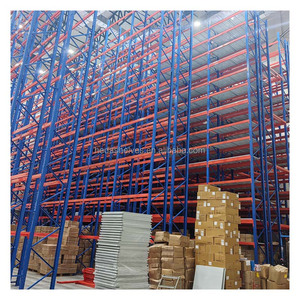
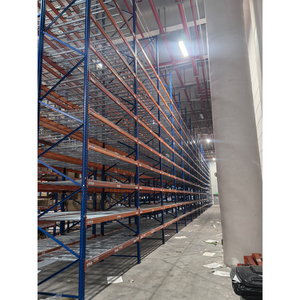
In high-bay racking systems (spanning heights from 6 meters to over 30 meters in ASRS applications), column profile design dictates lateral rigidity. Advanced continuous cold-roll forming lines produce multi-ribbed column upright profiles (e.g., 80×60mm, 90×70mm, 100×70mm, 120×95mm) with wall thicknesses ranging from 1.5mm to 3.0mm. Combined with precision-engineered box beams or step beams joined via 3-hook or 4-hook drop-in connectors with automatic safety locks, these systems deliver optimal buckling resistance and safety margins.
Finite Element Analysis (FEA)
Prior to manufacturing, engineering drawings undergo 3D Finite Element Analysis to simulate maximum point loads, seismic ground acceleration (Zone 1 through Zone 4 compliance), and frame sway limits under extreme operational conditions.
Surface Finishing & Corrosion Resistance
Automated 9-stage pre-treatment washing followed by thermo-set epoxy polyester powder coating (60–80 microns thickness) or hot-dip galvanizing (HDG according to ISO 1461) ensures superior protection against humidity, chemicals, and sub-zero temperatures.
OEM/ODM Custom Profile Roll-Forming
Custom beam profiles, teardrop hole punch patterns for North American compatibility, European 50mm pitch adjustable uprights, and special heavy-load footplates engineered to match specific slab load tolerances.
Custom Pallet Racking Architecture Comparison
Selecting the optimal racking system based on SKU density, pallet selectivity, forklift dynamics, and total cost of ownership (TCO).
| Racking System Type | Storage Density | Pallet Selectivity | Stock Rotation | Primary Industrial Application | Ideal Floor Height |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | FIFO / LIFO | E-commerce fulfillment, 3PL logistics, retail distribution | 3m – 12m |
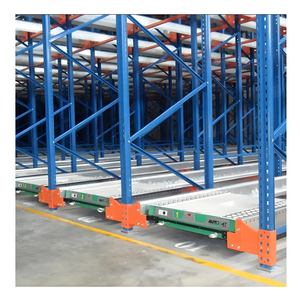
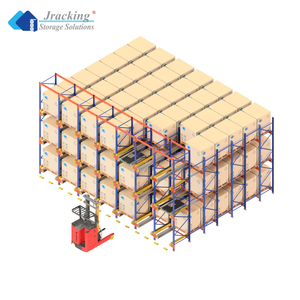
| Radio Shuttle Racking | High (75-85%) | Lane Dependent | FIFO or LIFO | Cold storage, food & beverage, high-volume fast-moving SKUs | 4m – 18m |
| Very Narrow Aisle (VNA) | High (65-75%) | 100% Direct Access | FIFO / LIFO | High-density archives, pharmaceutical logistics, premium space facilities | 6m – 15m |
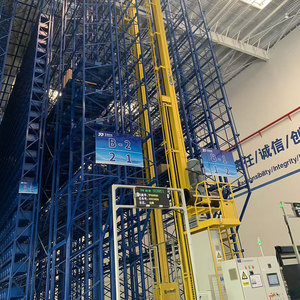
| Automated 4-Way Shuttle (ASRS) | Ultra-High (85-95%) | Automated WCS/WMS | Dynamic FIFO | Smart automated factories, 24/7 cold chain, high-bay automated hubs | 6m – 35m+ |
| Drive-In / Drive-Through Rack | Very High (70-80%) | Low (Block Storage) | LIFO (Drive-In) / FIFO | Seasonal bulk goods, uniform SKUs, chemical manufacturing | 4m – 12m |
| Push-Back & Pallet Flow | High (60-70%) | Per Lane (2–6 Deep) | LIFO (Push) / FIFO (Flow) | Buffer inventory, order consolidation, perishable goods handling | 3m – 10m |
Need a Custom Warehouse CAD Design & Quote?
Our structural engineers will analyze your floor plan, pallet dimensions, forklift turn radius, and load weights to provide a complete 2D/3D layout design and factory-direct quotation within 24 hours.
Send an InquiryFuture Procurement Trends in Industrial Storage (2026–2030)
Key technical shifts driving global warehouse infrastructure procurement and factory equipment choices.
1. Convergence of Static Racks with Robotics & AMR Integration
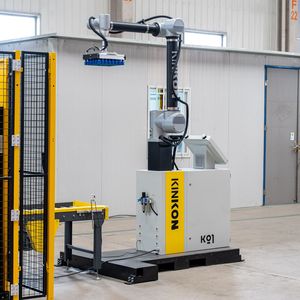
Traditional static pallet racks are rapidly being adapted to support Autonomous Mobile Robots (AMRs), Collaborative Robot Palletizers, and 4-Way Radio Shuttles. Modern Chinese manufacturers are building racks with precision laser-aligned rail tracks, integrated power charging docks, and photo-electric sensor brackets directly into the beam profiles, enabling seamless transition from manual forklift operation to fully automated smart warehousing.
2. Green Steel Sourcing & Low-Carbon Manufacturing
ESG compliance is becoming a critical procurement gatekeeper for multinational corporations. Leading Chinese racking factories are transitioning toward recycled scrap steel processing, zero-VOC electrostatic powder coating technologies, and solar-powered manufacturing plants to drastically cut the Scope 3 embodied carbon footprint per steel racking component exported to Europe and North America.
3. Ultra-Dense Cold-Chain Thermal Optimization
With global cold chain logistics expanding rapidly for biological products, frozen foods, and vaccines, storage density per cubic meter dictates operational profit margins. High-density shuttle systems and mobile rack systems operating reliably down to -30°C are replacing standard selective racks, reducing electrical refrigeration power consumption per pallet slot by up to 40%.
4. Modular Scalability & Rapid Assembly Connectors
Global logistics demand dynamic layout flexibility. Boltless connection systems, pre-assembled upright frames, and standardized step beam profiles allow end-users to reconfigure beam levels in 50mm or 75mm increments without structural welding or specialized tools, significantly shortening site installation windows.
Industry Development Trends in Racking Manufacturing
How China's industrial racking ecosystem is evolving to deliver high-precision engineering on a global scale.
Automated Roll-Forming Lines & Robotic Welding Precision
The manufacturing process for industrial racking has underwent a monumental transformation over the past decade. Modern production bases in Nanjing, Jiangsu, and nearby industrial hubs utilize fully automated continuous roll-forming production lines integrated with flying shear punching systems. This technology ensures hole pitch tolerances within ±0.1mm across a 12-meter upright post.
Robotic welding arms now execute 100% of beam connector plate welds. Automatic double-sided welding guarantees complete penetration along beam seams, eliminating manual human welding fatigue flaws and providing structural yield strength that consistently surpasses standard load-bearing requirements. Furthermore, continuous digital ultrasonic flaw detection is deployed on structural welds for heavy-duty ASRS stacker crane guide rails and heavy load cantilever arms.
Why Partner with Remprack Storage Solutions?
Over two decades of structural engineering excellence, global export logistics expertise, and custom factory manufacturing.
20+ Years Manufacturing Heritage
Established in 2006 in Nanjing, China, Remprack has grown into a world-class racking equipment manufacturer with over 2,000 successful warehouse installations delivered across 85+ countries worldwide.
International Certification Compliance
All Remprack systems hold full certification under ISO 9001:2015 Quality Management, ISO 14001 Environmental System, European CE Certification, and TUV Rheinland structural load testing standards.
Custom Engineering & 10-Year Warranty
We back our structural design integrity with a 10-Year Comprehensive Warranty. Our in-house engineering lab holds over 100 patents in shuttle mechanisms, beam locking devices, and seismic rack baseplates.
Frequently Asked Questions (FAQ) for Global Buyers
Direct technical answers regarding layout design, structural safety standards, custom OEM manufacturing, and export shipping logistics.
Ready to Upgrade Your Warehouse Efficiency?
Connect directly with our senior structural engineers today for technical consultation, free CAD layout engineering, and factory-direct price estimates.
Send an Inquiry