Featured Industrial & Mobile Racking Products
Explore our certified range of high-capacity storage rack systems, engineered for selective access, extreme ambient durability, and maximum floor density.
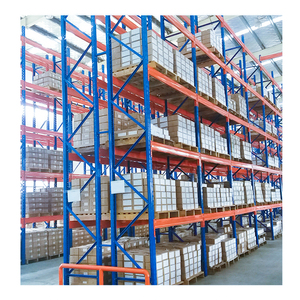
Certificated Large Heavy Duty 5 Steel Shelving Storage Applications Easy Assemble Racking Unit Industrial Pallet Rack Solution
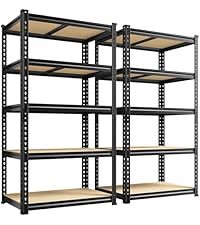
5 Layer Industrial Storage Shelving Racks Heavy Duty Adjustable Boltless Rivet Rack Corrosion Protection Warehouse Powder Coated
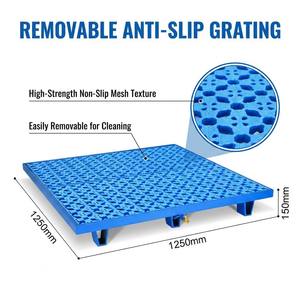
Industrial Movable Leak-Proof Corrosion Protected VNA Pallet Rack Heavy-Duty Metal Plastic Construction Forklift Compatible
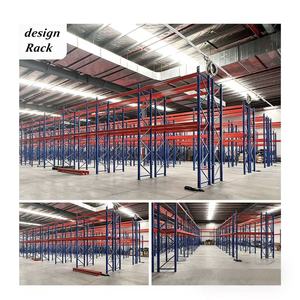
Certificated Bolted Heavy Duty Industrial Forklift Stacking Rack Selective Shelves Storage Rack Pallet Racking
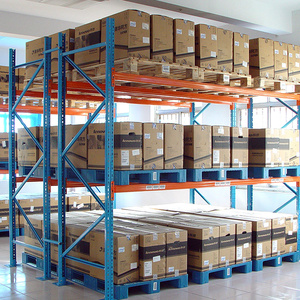
Favorable Price High Quality Heavy Duty Warehouse Storage Rack Industrial Selective Racks for Food Cold Room
Customized Heavy Duty Industrial Storage Shelves System Metal Rack Stacking Units Warehouse Steel Industrial Pallet Racking
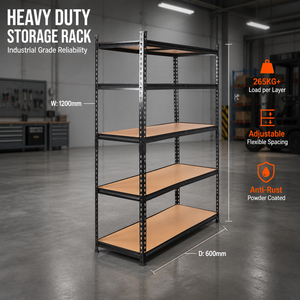
Heavy Duty Steel Shelving Rack Boltless Storage Shelves 5 Tier Adjustable Metal Garage Warehouse Industrial Shelf Racking
Heavy Duty Storage Rack Pallet Rack System Shelf For Industrial Storage Rack
Custom OEM Mobile Storage Racking Engineering & Factory Capabilities
An architectural evaluation of motorized mobile pallet racking systems, structural integrity parameters, cold room thermodynamic efficiencies, and global OEM/ODM manufacturing standards.
Volumetric Storage Maximization
Conventional selective pallet racking dedicates up to 60% of floor space to operating aisles. Motorized Mobile Racking Systems (Electrical Mobile Racking) eliminate static aisles by mounting rack frames onto electronically controlled mobile bases running on embedded floor rails. A single operational aisle is dynamically opened only when requested, expanding total usable warehouse pallet storage capacity by up to 85% to 100% within the existing building footprint.
Structural Q355B Steel Mechanics
High-density mobile storage racks require rigorous finite element analysis (FEA) to endure dynamic acceleration, braking torque, and structural load shifting. Our OEM manufacturing facility utilizes high-tensile Q355B/Q235B cold-rolled structural steel for upright columns and beam profiles, engineered strictly according to European FEM 10.2.07 structural codes and EN 15512 standards. Each mobile base is equipped with heavy-duty forged steel wheels and direct-geared motor drives.
Cold Storage Thermal Optimization
In refrigerated and deep-freeze logistics (-30°C), cubic meter energy costs are exceptionally high. Mobile storage racking reduces the cooling cube requirement by consolidating pallets into a compact block. Our custom OEM cold-room mobile racks feature low-temperature synthetic lubricants, anti-condensation PLC control enclosures, IP65-rated motors, and specialized steel alloys to prevent low-temperature hydrogen embrittlement.
Structural Architecture & System Performance Parameters
Comparative engineering matrix between conventional racking and customized motorized mobile rack installations.
| Performance Metric | Selective Pallet Racks | Drive-In Racking | Motorized Mobile Racking (OEM Custom) | 4-Way Automated Shuttle |
|---|---|---|---|---|
| Floor Utilization Efficiency | 35% - 45% | 65% - 75% | 80% - 90% | 85% - 95% |
| Pallet Selectivity | 100% Direct Access | Low (LIFO Block Storage) | 100% Direct Access (Aisle Opened) | High (WMS Controlled) |
| Max Bay Load Capacity | Up to 15,000 kg | Up to 12,000 kg | Up to 24,000 kg per base | Up to 1,500 kg / pallet |
| Cold Storage Operating Temp | -30°C to +45°C | -30°C to +45°C | -30°C to +40°C (IP65 Enclosed) | -25°C to +40°C |
| Safety & Anti-Collision | Passive Upright Protectors | Guide Rails | Multi-level Photoelectric Light Curtains | Integrated Obstacle Radar |
| Capital Investment ROI | Baseline | Moderate | Rapid (18-24 Months in Cold Chain) | Long-Term Advanced Automation |
Future Procurement Trends in Mobile Storage Racking Systems
As global supply chains shift toward urban fulfillment hubs, automated cold storage, and ESG energy mandates, procurement teams must evaluate mobile storage racks based on four emerging industrial trends.
1. Integration of Smart Warehouse Management Systems (WMS) & IoT
Modern procurement specifications no longer view mobile racks as static steel hardware. Future procurement standardizes on mobile racking bases integrated with Siemens or Allen-Bradley PLCs via Industrial Ethernet or PROFINET interfaces. This enables RF-remote automatic aisle opening, night-option spacing (for uniform cold air circulation), and pre-positioning algorithms synced directly with automated forklift truck (AGV) guidance systems.
Get a Quote2. Net-Zero Carbon Goals & Refrigeration Energy Reduction
Energy consumption in cold storage facilities accounts for up to 60% of operational overhead. By deploying custom mobile racking, enterprise buyers cut total refrigeration volume requirements by nearly half while maintaining identical pallet counts. Procurement officers are leveraging this footprint reduction to secure green warehouse certifications (LEED / BREEAM) and offset industrial power surcharges.
Get a Quote3. Advanced Multi-Layer Safety Protocols (ISO 13849-1 Compliance)
Safety standards for motorized equipment are becoming significantly stricter across Europe, North America, and Australia. Procurement specs require PL d/Category 3 safety circuits, optical safety light barriers along moving bases, floor-level emergency stop bars, manual override switches, and acoustic/visual movement beacons to guarantee zero risk to personnel and forklift operators inside open aisles.
Get a Quote4. Modular OEM Customization & Floor-Flatness Engineering
Procurement teams are moving away from rigid standard catalogs toward OEM factories capable of bespoke rack profile engineering. Modern mobile racking orders prioritize low-profile, surface-mounted or floor-embedded precision steel rails (flatness tolerance according to VDMA 36610 or DIN 15185) that allow seamless conversion of standard warehouses without deep concrete slab re-trenching.
Get a QuoteFuture Product Development Trends in Mobile Racking Systems
How structural design, automation, dynamic safety, and mechanical engineering are shaping the next generation of custom mobile storage solutions.
Autonomous Mobile Robot (AMR) Alignment
The next generation of mobile racking systems is engineered specifically to interface with driverless forklifts and Autonomous Mobile Robots (AMRs). Integrated sensor arrays communicate rack carriage positioning to fleet management software, ensuring AMRs enter open aisles with millimeter-precise laser navigation.
Seismic-Resilient Base Engineering
With warehouses expanding in seismic regions (such as the Pacific Rim, Southern Europe, and Latin America), R&D is focused on anti-tilt guide mechanisms, top-guide stability beams, dynamic brake locks, and seismic base anchors adhering to Eurocode 8 and FEMA 460 guidelines to prevent rack collapse during earth tremors.
Self-Diagnostic Predictive Maintenance IoT
Factory-installed IoT vibration sensors, motor thermal monitoring, and cycle counter modules are transforming mobile storage maintenance. Maintenance teams receive real-time warnings regarding wheel alignment wear, rail debris obstruction, or gear oil degradation before any unscheduled operational downtime occurs.
Why Partner with Remprack Storage Solutions for Custom OEM Manufacturing?
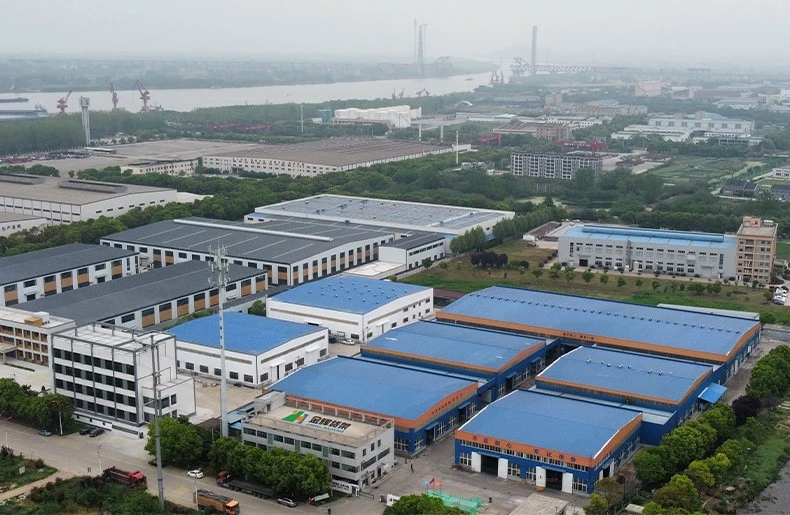
Since 2006, Remprack Storage Solutions Co., Ltd. has established itself as a premier China-based factory for heavy-duty pallet racking, shuttle systems, cantilever storage, and motorized mobile racking solutions.
Fully Integrated 40,000 m² Manufacturing Facility
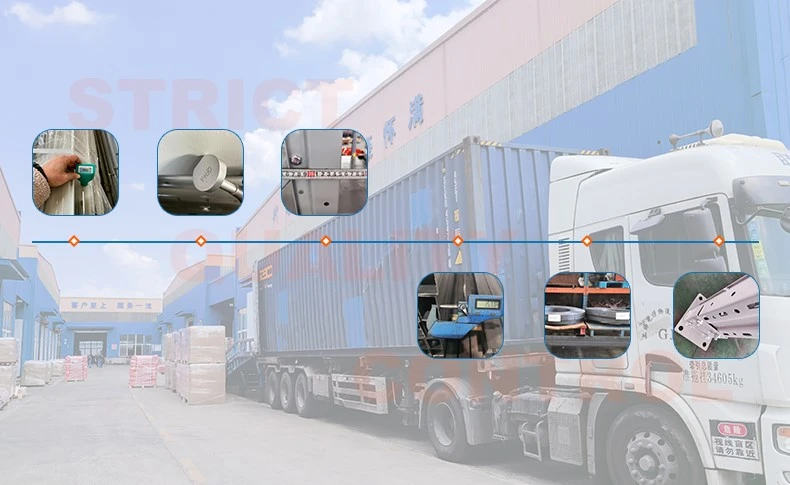
Our modern manufacturing plant in Nanjing, China, houses continuous high-precision cold roll-forming lines, robotic welding stations, laser beam cutting, and automated continuous electrostatic powder-coating lines. We control raw steel purchasing (grade Q235B & Q355B from Baosteel), cold forming, punching, surface treatment, and testing completely in-house to ensure uncompromised quality and direct factory pricing.
International Certification Framework (CE, ISO, TUV)
Our production operations and structural designs comply with global standards. Remprack holds official certifications for CE, ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and TUV Rheinland performance verification. Complete raw material mill certificates, load test reports, and structural safety calculations are supplied with every project export.
Complete OEM & ODM Customization Support
We partner directly with storage equipment distributors, system integrators, rack dealers, and general contractors worldwide. Upright column profiles, step/box beam dimensions, beam connector claw configurations, customized RAL powder-coating colors, private label branding, and customized packaging are fully supported to match regional market specifications.
OEM / ODM Project Execution Workflow
How our technical engineering department delivers custom mobile racking projects from initial drawing to final commissioning.
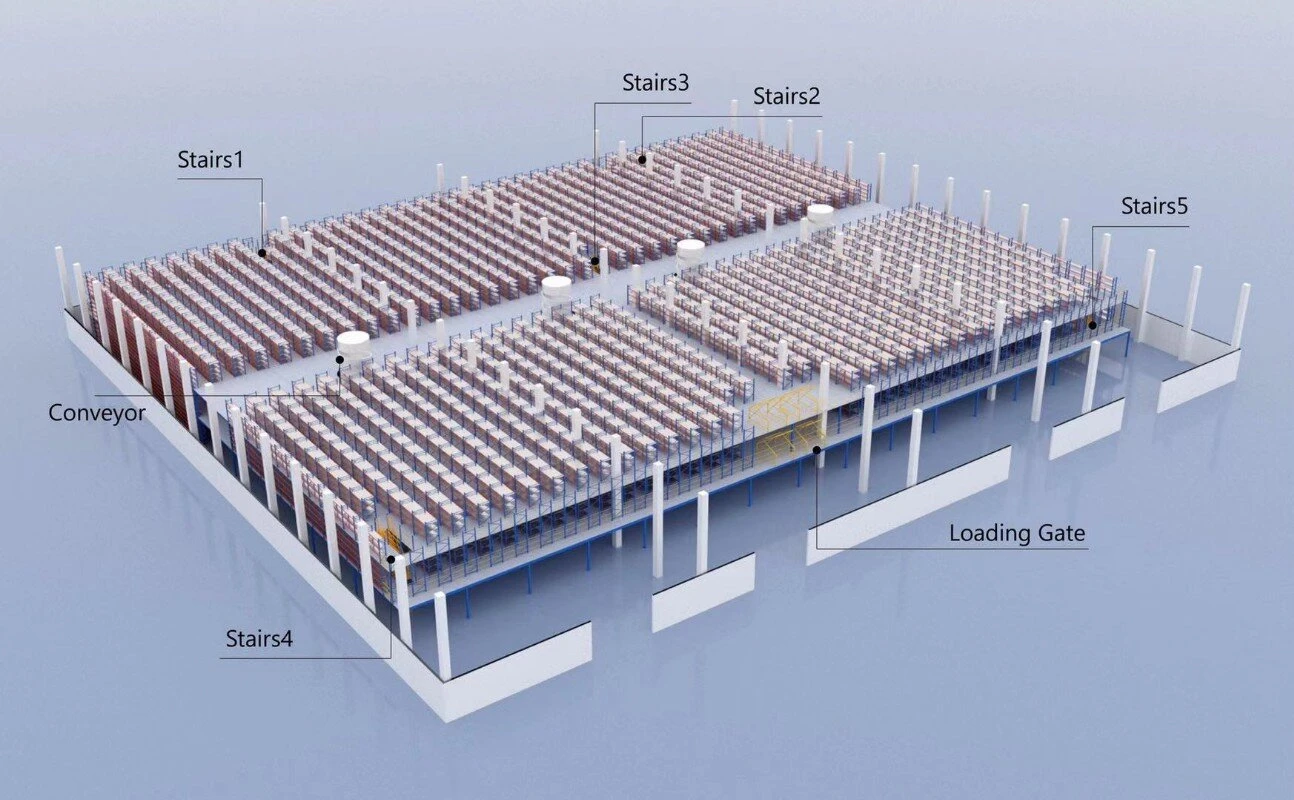
CAD Layout & Data Review
Analyzing warehouse floor plans, height clearance, pallet sizes, unit weights, and forklift specifications.
Structural FEA Design
Calculating static/dynamic load capacities, column stability, and rail embedment depth requirements.
Commercial Proposal
Itemized FOB/CIF quotation, raw material specifications, steel grade confirmation, and lead-time schedule.
Intelligent Manufacturing
Roll-forming uprights, robotic welding of beam connectors, surface shot-blasting, and powder coating.
QC & Export Packaging
Ultrasonic weld inspection, powder thickness test, steel band bundling, and container loading optimization.
Site Installation Support
Supplying detailed CAD installation assembly drawings, anchor bolt layouts, and online engineering guidance.
Frequently Asked Questions (FAQ) - Mobile Racking Procurement
Detailed engineering and commercial answers to frequent technical queries from logistics engineers, warehouse managers, and B2B buyers.
Transform Your Warehouse Density with Custom OEM Mobile Storage Racks
Contact our senior warehouse engineering team today. Send us your floor plan CAD file or project specification to receive a complimentary custom layout design, structural FEA calculation, and competitive factory-direct OEM quote.