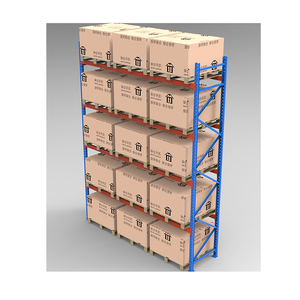
Custom OEM Heavy Duty Product Portfolio
Explore engineered heavy-duty racks, selective storage frames, and high-load steel racking direct from our factory.
China Factory Price Steel Selective Heavy Duty Storage Racking Industrial Rack Shelving Pallet Rack
Jracking Australian Standard Industrial Racks CE Certified Heavy Duty Pallet Racking System for Warehouse
Chinese Manufacture Heavy Duty Metal Pallet Rack Shelving Wood Pallet Racks And Shelves
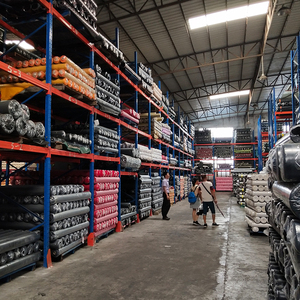
Highly Customizable Free Design Storage Rack for Various Heavy Duty Storing 1000KG 2000KG 3000KG
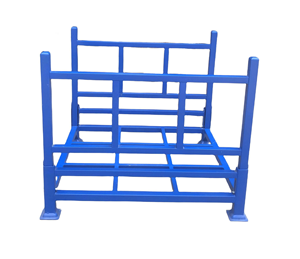
Customized Heavy-Duty Blue Steel Warehouse Shelves Folding Pallet Racking Anti-Corrosion
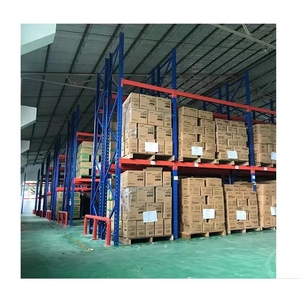
Heavy Duty Industrial Metal Shelving Certificated Pallet Storage Shelves Warehouse Racking
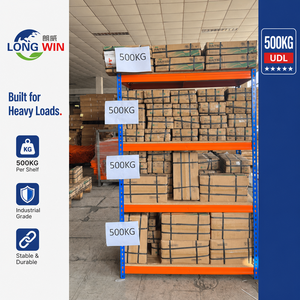
Extra Heavy Duty Boltless Steel Rack 5-Tier Adjustable 2000kg Rivet Lock Warehouse Rack
Engineering Excellence & Manufacturing Capacity
Remprack Storage Solutions Co., Ltd. brings 20+ years of dedicated structural steel engineering expertise.
2006
Established Year
40,000 m²
Smart Production Base
100+
Patented Technologies
85+
Global Export Countries
Industrial Steel Racking Infrastructure Engineered for Extreme Loads
Modern logistics hubs, cold chain centers, and industrial manufacturing plants require extra heavy-duty racking systems capable of bearing high dynamic and static loads without elastic deformation. Standard off-the-shelf racking frequently fails to meet rigorous seismic safety factors or localized deflection limitations (such as L/200 or L/300 standard constraints).
As a leading China OEM/ODM factory established in 2006, Remprack operates a 40,000 m² state-of-the-art facility equipped with high-precision cold roll-forming lines, robotic welding stations, and automated electrostatic powder coating lines. Our structural designs strictly adhere to international codes including AS4084-2012 (Australian Standard for Steel Storage Racking), FEM 10.2.02 (European Federation of Materials Handling), and ANSI/RMI MH16.1.
| Structural Feature | Remprack Extra Heavy Duty Standard |
|---|---|
| Steel Grade | Certified Q235B / Q355B High Yield Tensile Cold Rolled Steel |
| Load Capacity / Level | 1,000 kg up to 4,000 kg per beam pair (Customizable) |
| Upright Profiles | Omega profile, 80/90/100/120/140mm width with multi-bend ribs |
| Beam Connections | 3 or 4-hook heavy duty interlock connectors with mechanical safety pins |
| Surface Treatment | Epoxy Powder Coating (60-80μm) or Hot-Dip Galvanized (ISO 1461) |
| Compliance Certification | CE, ISO 9001, ISO 14001, TUV Rheinland Certified |
Strategic Engineering & Custom OEM Manufacturing
Unlocking information gain: understanding structural parameters, stress analysis, and structural integrity.
Advanced Structural Finite Element Analysis (FEA)
Every custom extra heavy-duty pallet rack engineered by Remprack undergoes rigorous computerized FEA simulations to analyze load distributions under static, dynamic, and seismic conditions.
- Elimination of localized stress concentration points across beam-to-upright joints.
- Seismic bracing calculation tailored to local geological acceleration coefficients.
- Deflection limit verification strictly held under 1/200th of the span distance.
Precision Cold Roll-Forming & Metallurgy
Structural reliability starts with raw materials. We utilize prime certified steel coils from premium mills, ensuring high structural ductility and zero surface micro-fractures during forming.
- Multi-stage continuous roll-forming ensures consistent profile cross-sections.
- Upright pitch adjustment every 50mm, 75mm, or 76.2mm (3 inches) for flexible levels.
- Custom punched pattern formats: Teardrop, Hexagonal, and Diamond keyhole connection.
Anti-Corrosion & Heavy-Duty Finishes
Operating environments vary from humidity-controlled pharmaceutical warehouses to sub-zero cold stores and corrosive chemical facilities.
- Pre-treatment 9-stage phosphate wash ensures maximum paint adhesion.
- Thermosetting epoxy powder coating delivers high impact and wear resistance.
- Hot-Dip Galvanized option for outdoor yards or harsh chemical atmospheres.
Future Procurement & Product Development Trends (2025–2030)
Key insights for supply chain directors, warehouse integrators, and B2B procurement managers.
1. Convergence of Heavy-Duty Frames with Automation (ASRS & 4-Way Shuttles)
Future industrial warehouses are transitioning away from traditional forklift-only selective racking toward hybrid automated infrastructure. Heavy-duty pallet racks are no longer passive steel frameworks; they serve as structural guides for high-speed Radio Shuttles, Automated Guided Vehicles (AGVs), and ASRS Stacker Cranes.
Procurement teams must specify tighter manufacturing tolerances (e.g., ±0.5mm overall rack alignment accuracy) to prevent automated shuttles from jamming during high-density operations.
2. Modular Reconfigurability & Circular Supply Chain Demands
Rapid changes in e-commerce SKUs and pallet dimensions demand modular OEM racking that can be expanded horizontally or vertically without requiring complete structural tear-downs. Multi-tier mezzanine integration and adjustable boltless beam connections allow facilities to double usable space within existing building footprints.
3. Decarbonization & Low-Carbon Steel Compliance
Global buyer guidelines increasingly mandate supply chain emissions tracking. OEM racking suppliers are expected to provide environmental product declarations (EPDs) and utilize green steel production methods, combined with VOC-free powder coating technologies to support net-zero building certifications (LEED / BREEAM).
4. IoT-Integrated Structural Health Monitoring
The integration of digital strain gauges and impact sensors into rack uprights is emerging as a critical trend. Smart racking systems notify facility managers of forklift impact events in real-time, allowing preventative maintenance before structural buckling or catastrophic collapse occurs.
Why Partner with Remprack Storage Solutions?
Comprehensive OEM/ODM capabilities trusted by warehouse integrators across 85+ countries.
Free Engineering Design & CAD Layouts
Our in-house design team provides custom structural calculations, 2D floor plans, and 3D architectural renderings tailored to your specific building column grid, door positions, and forklift turning radius.
Full In-House Manufacturing Control
From raw coil slitting to cold roll-forming, robotic welding, surface coating, and export bundling—every stage is monitored under our strict ISO 9001 quality management system with full batch traceability.
Global Export Experience & 10-Year Warranty
With thousands of successful logistics projects completed in Europe, North America, the Middle East, and Southeast Asia, we back our structural racking with an industry-leading 10-year warranty.
Extra Heavy Duty Pallet Racking - Procurement FAQ
Detailed technical answers to standard buyer inquiries and structural engineering questions.
What data is required to generate a custom structural racking design and quote?
To prepare an accurate structural layout and load quotation, our engineering team requires: (1) Warehouse floor plan in CAD or PDF showing clear height under eaves and sprinklers; (2) Pallet dimensions (W x D x H) including goods overhang; (3) Maximum weight per loaded pallet (e.g., 1000kg, 2000kg, 3000kg); (4) Forklift specifications (minimum aisle width requirement, maximum lift height, and mast height); (5) Operating temperature range and local seismic requirements.
How do OEM extra heavy-duty pallet racks differ from standard duty selective racks?
Extra heavy-duty pallet racks utilize thicker gauge steel (ranging from 2.0mm up to 3.5mm), wider upright profiles (90mm to 140mm face width) with internal strengthening ribs, and specialized box/step beams with heavy-duty multi-claw connectors. Standard duty racks typically top out at 1,000kg–1,500kg per beam level, whereas extra heavy-duty systems comfortably support 2,000kg up to 4,000kg per level under strict deflection limits.
What international safety standards do Remprack racking systems comply with?
Remprack racking systems are fully engineered and tested in accordance with AS4084-2012 (Australian Standard), FEM 10.2.02 (European Code), and ANSI/RMI MH16.1. Our factory holds ISO 9001 (Quality Management), ISO 14001 (Environmental Management), CE certification for European structural safety, and TUV Rheinland factory inspection verification.
Can we customize color schemes, upright profile punching, and branding for OEM orders?
Yes. As a direct OEM factory supplier, we offer complete customization. You can select custom RAL colors for powder coating (e.g., standard RAL 5015 Blue, RAL 2004 Orange, or custom brand colors), select custom hole-punching pitch (50mm, 75mm, 76.2mm), and request OEM branding decals or stamped logos on beam connectors and load plates.
What surface treatment should be chosen for cold storage or outdoor facilities?
For standard ambient warehouses, high-durability electrostatic epoxy powder coating (60–80 microns) provides excellent scratch and chemical resistance. For sub-zero cold stores with high humidity condensation or outdoor storage yards, we strongly recommend Hot-Dip Galvanizing (HDG) compliant with ISO 1461, which coats both internal and external steel surfaces with a protective zinc layer resisting rust for decades.
How are extra heavy-duty pallet racking components packaged for ocean freight?
All upright frames and beams are tightly bundled using heavy-duty steel strapping and wrapped in protective plastic film with wooden dunnage corners to prevent transit friction. Small components, floor anchor bolts, shims, and safety pins are packed in reinforced wooden crates or export cartons to ensure 100% complete arrival without damage.
Transform Your Warehouse Storage Infrastructure Today
Contact our structural engineers for a complimentary layout evaluation, load calculation, and competitive factory-direct quote within 24 hours.
Get a Quote