Precision-Engineered Pharmaceutical Racking Portfolio
Direct OEM/ODM Solutions for Bulk Raw Materials, APIs, Cold Chain Storage, and Automated Distribution Hubs
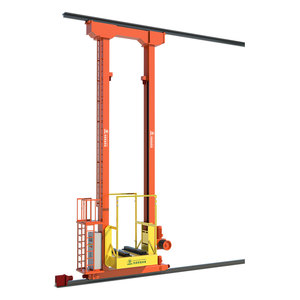
Automatic Pallet Stacker Crane Racking System
Intelligent steel warehouse racking with anti-corrosion protection designed for automated high-bay pharmaceutical storage.
Get Catalog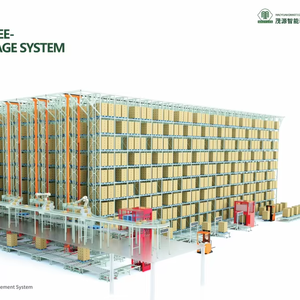
Goods Shelves for Four-Way Shuttle Warehouse
Ultra-dense storage grid compatible with 4-way robotic shuttles, ideal for cold-chain pharmaceutical distribution.
Get Catalog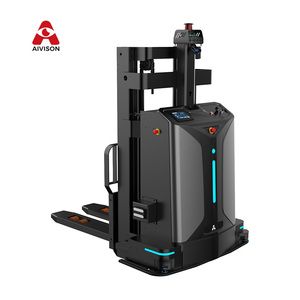
Autonomous Mobile Robot (AMR) AGV Pallet System
AGV forklift integration racking designed for automated pallet handling in cleanroom and production environments.
Get Catalog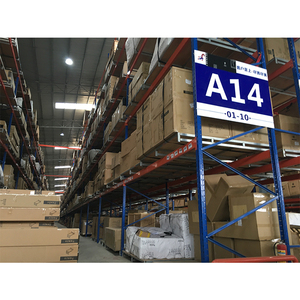
Boltless Heavy Duty Beam Rack
Sturdy structural steel pallet shelving engineered for factory warehouses and pharmaceutical distribution hubs.
Get Catalog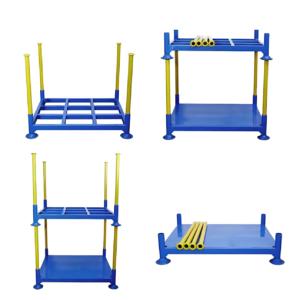
OEM Customized Folding Movable Pallet Rack
Detachable and portable stacking frames offering modular flexibility for temporary chemical & pharma staging.
Get Catalog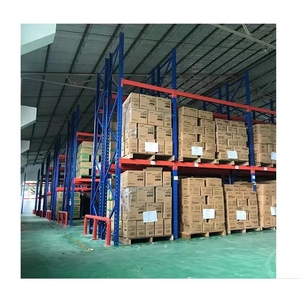
Heavy Duty Industrial Certified Pallet Shelves
CE and TUV-certified heavy industrial racking optimized for bulk raw material handling and containerized storage.
Get Catalog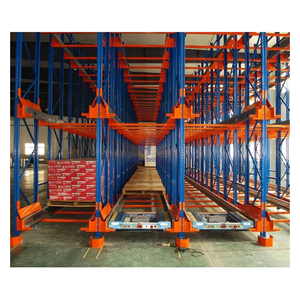
Customized Automatic Shuttle Pallet System
High-density automated storage shuttle system engineered for maximum volumetric efficiency in temperature-controlled facilities.
Get Catalog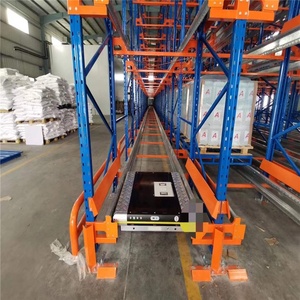
Automated Radio Shuttle Car & Cart System
Radio-controlled pallet shuttle cart executing deep-lane storage operations with minimal operator intervention.
Get Catalog1. Executive White Paper: The Role of Advanced Storage Infrastructure in Modern Pharmaceutical Supply Chains
The global pharmaceutical supply chain demands stringent regulatory compliance, strict thermal tracking, zero-contamination operational environments, and flawless inventory traceability. Storage infrastructure is no longer merely static steel frames; it serves as a critical control point within Good Manufacturing Practice (GMP) and Good Distribution Practice (GDP) frameworks.
When procurement officers, facility engineers, and warehouse logistics directors evaluate China wholesale pharmaceutical pallet racking factories and exporters, technical compliance takes precedence over initial capital cost. Structural integrity under seismic load, surface finish cleanability, cold-chain thermal air displacement, and seamless integration with Automated Storage and Retrieval Systems (AS/RS) define the benchmark for top-tier storage solutions.
Core Technical Directive: Pharmaceutical pallet racking systems must withstand structural stresses up to safety factor 1.5 while providing micro-smooth powder-coated or galvanized surface finishes (resistive to aggressive chemical sanitizers including isopropyl alcohol, hydrogen peroxide vapor, and chlorine-based cleanroom agents).
From Active Pharmaceutical Ingredient (API) raw material storage requiring explosion-proof dynamic load configurations, to cold-chain biologics requiring -30°C static stability, structural steel design directly influences operational safety, product stability, and audit outcomes by regulatory bodies such as the US FDA, EMA, and NMPA.
2. Structural Engineering & Metallurgy Standards for Pharma-Grade Racking
China's leading export-oriented racking manufacturers utilize high-grade certified cold-rolled structural steel (primarily Q235B and Q355B structural steel grades equivalent to S235JR and S355JR under European EN 10025 standards). Steel profiles undergo high-precision continuous roll-forming to ensure uniform thickness and eliminate stress concentrations.
2.1 Load Distribution & Seismic Deflection Limits
Engineering compliance follows international design codes including the Rack Manufacturers Institute (RMI) specification, ANSI MH16.1, and European FEM 10.2.02 standards. Key engineering metrics include:
- Maximum Beam Deflection: Restricted to L/300 under full design load (where L is clear beam length), preventing binding on automated shuttle rails and stacker crane forks.
- Safety Factor on Structural Members: Minimum 1.65 dynamic safety coefficient relative to yield strength.
- Seismic Base Plate Anchor Systems: Heavy-gauge footplates connected via expansion or chemical anchors designed according to local ground acceleration spectrums (Zone 1 through Zone 4 seismic ratings).
2.2 Surface Finishing Technology: Cleanroom & Anti-Corrosion Compliance
To eliminate particle shedding and prevent microscopic microbial harboring, pharmaceutical pallet racks undergo multi-stage automated surface treatment:
Automated Pre-Treatment
Phosphate wash and alkaline degreasing remove all oils, followed by deionized water rinses to guarantee maximum surface tension for powder coating adhesion.
Electrostatic Epoxy-Polyester Coating
Applied at 60 to 90 microns thickness. Cured at 200°C to form a non-porous, highly scrubbable polymer barrier that withstands daily sanitization.
Hot-Dip Galvanizing (HDG)
Optional zinc coating (ISO 1461 compliant, 65–85 microns) designed for sub-zero cold storage rooms (-30°C) to eliminate rust formation caused by thermal cycling condensation.
3. Comparative Matrix: Selecting the Right System for Pharmaceutical Logistics
Different pharmaceutical product categories require tailored rack architectures. The matrix below provides an operational comparison for facilities engineers and buyers:
| Storage System Type | Density Level | Pallet Access (FIFO / LIFO) | Cold Storage Suitability | Automation Readiness | Primary Pharma Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (100% Selectivity) | 100% Direct Access (FIFO/LIFO) | Moderate | Manual / AGV Docking | Finished Goods Hubs, High SKU Variety |
| Radio Shuttle Racking | High Density (Deep-Lane) | Configurable (FIFO or LIFO) | Excellent (-25°C to -30°C) | Semi-Automated Robotic Shuttle | Cold Chain Vaccines, High-Volume Biologics |
| 4-Way Shuttle ASRS | Ultra-High Density | Fully Dynamic (WMS-Driven FIFO) | Outstanding | Fully Automated (AS/RS + AMR) | 24/7 Automated Pharma Distribution Centers |
| Drive-In Racking | High Density | Strict LIFO | Good | Manual Forklift Entry | Bulk API Staging, Batch Production Buffers |
| Gravity Pallet Flow | High Density | Strict Gravity-Fed FIFO | Good | Conveyor System Docking | Perishable Reagents, Expiry-Sensitive Stock |
4. Sourcing & Future Procurement Trends in China Racking Manufacturing (2025–2030)
Global procurement directors sourcing from China wholesale pharmaceutical pallet racking factories are navigating major technological and environmental shifts. Over the next decade, three dominant trends will shape global procurement strategies:
4.1 Shift Toward Fully Automated 4-Way Shuttle & AS/RS Systems
Labor cost inflation, combined with strict cleanroom human exclusion protocols, is driving global pharmaceutical operators toward total automation. Racking designs have evolved from passive load holders into structural guiding tracks for 4-way robotic shuttles and stacker cranes. Tolerance limits for upright straightness have dropped to less than 1 mm per 3 meters of vertical height, requiring continuous automated laser manufacturing lines.
4.2 Thermal Optimization for Cold-Chain Energy Conservation
Energy consumption in sub-zero refrigerated storage represents up to 40% of overall facility operating costs. High-density shuttle racking systems eliminate unnecessary aisle space, increasing storage capacity per cubic meter by up to 80%. This reduced footprint directly minimizes cooling envelope requirements and lowers carbon footprints.
4.3 Digital Twin Integration & Structural Health Monitoring
Future-ready wholesale racking factories in China are incorporating smart strain gauges and IoT vibration sensors directly into structural upright bases. These integrated systems allow global warehouse operators to monitor structural integrity in real time, detecting accidental forklift impacts and dynamic load stresses via cloud dashboards.
5. Comprehensive Procurement & Engineering FAQ
6. Enterprise Capabilities & Manufacturing Advantage: Why Remprack
Founded in 2006, Remprack Storage Solutions Co., Ltd. (Nanjing, China) operates a modern 40,000 m² production facility equipped with high-speed automatic cold roll-forming machines, robotic laser welding stations, and an automated continuous powder-coating line. With over 20 years of focus on heavy-duty industrial storage, Remprack has successfully delivered 2,000+ projects across 85+ countries.
Comprehensive Quality Certifications
Certified under CE, ISO 9001:2015, ISO 14001 environmental management standards, and TUV load capacity verification, ensuring your project passes all third-party facility audits.
Factory Direct & 10-Year Warranty
Eliminate intermediary trade markups by sourcing directly from our factory floor. All structural steel racking components carry an industry-leading 10-year structural warranty.
Accelerate Your Pharmaceutical Warehouse Optimization Today
Connect directly with Remprack’s structural engineering team to receive customized CAD layouts, structural load calculations, and factory-direct price estimates within 24 hours.
Get Catalog