Featured Pallet Conveyor & Shuttle Storage Racking Systems
Direct factory manufacturing from Nanjing, China. Certified to CE, ISO 9001, ISO 14001, and TUV international structural engineering standards.
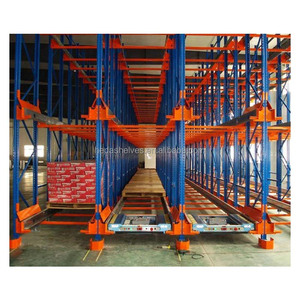
Auto Shuttle Racking System Innovative Pallet Racking Intensive Shuttle Racks Intelligent Cold Storage Shuttle Rack Automatic
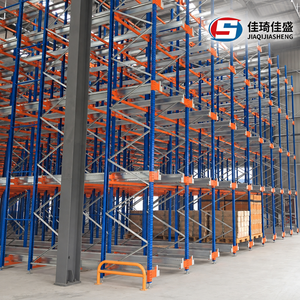
Multi-Level Automatic Warehouse Racking River-Type Pallet Two-way Radio Shuttle Rack for Storage Iron Steel Material
Steel Heavy Duty Racking High Density Pallet Racking Systems Warehouse Storage Racks for Sale
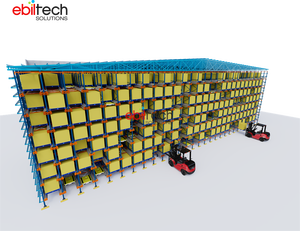
EBILTECH CE Certified Two Way Shuttle Clad Racking Warehouse Integrated Rack for Deep Lane Storage
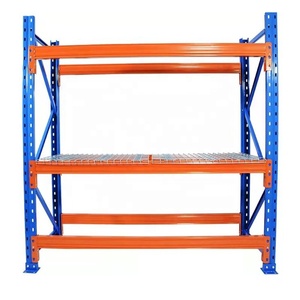
Q235B Steel Heavy Duty Selective Pallet Rack System Industrial Warehouse Beam Racking 2500kg Capacity Customized Storage
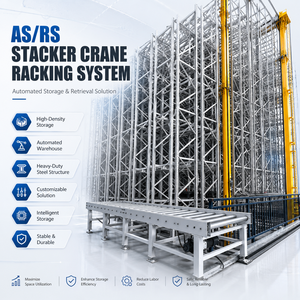
Automated ASRS Mezzanine Rack Stacker Crane Racking System High Density Warehouse Storage Heavy Duty Steel Pallet Rack OEM ODM
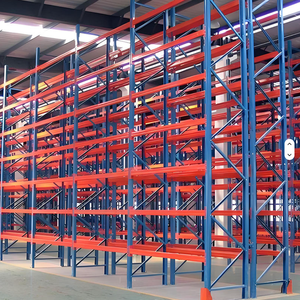
CE Industrial Rack Steel Metal Shelving Heavy Duty Warehouse Storage Racking System Selective Pallet Rack
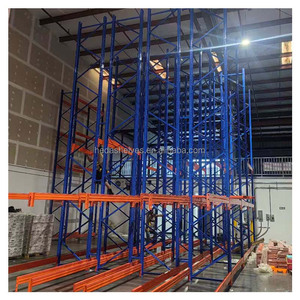
Custom Heavy-Duty 5-Layer Iron VNA Pallet Rack 1000KG-2000KG Capacity Adjustable Metal Stacking Shelving for Warehouse Storage
Engineering Architecture of Industrial Pallet Conveyor Storage Systems
An in-depth structural, mechanical, and operational evaluation for supply chain directors, logistics integrators, and procurement leaders.
In modern automated logistics and high-density material handling, pallet conveyor storage systems act as the structural backbone connecting automated receiving, high-bay racking storage, picking, and dispatch zones. As global supply chains transition toward Industry 4.0 standards, selecting a premier China pallet conveyor storage system manufacturer requires evaluating structural mechanics, steel grade compliance (Q235B/Q355B cold-rolled structural steel), drive mechanism efficiency, and integration compatibility with Warehouse Control Systems (WCS) and Warehouse Management Systems (WMS).
China's manufacturing ecosystem—centered in advanced industrial nodes such as Nanjing, Jiangsu—has evolved from basic structural rack fabrication into turnkey automated intralogistics engineering. Top-tier manufacturers like Remprack Storage Solutions (EBILTECH) engineer heavy-duty pallet handling systems capable of dynamically managing payload units ranging from 500 kg to over 2,500 kg per pallet position under extreme continuous duty cycles and harsh environmental operating conditions, including sub-zero cold storage down to -30°C.
Comparative Specification Matrix: Pallet Conveyor & Shuttle Media
Selecting the optimal transfer mechanism based on payload dynamics, throughput speed, structural deflection tolerances, and system integration complexity.
| Conveyor / Storage System Type | Max Unit Load (kg) | Transfer Speed (m/min) | Structural Steel Grade | Control Integration | Primary Application Zone |
|---|---|---|---|---|---|
| Heavy-Duty Motorized Roller Conveyor (MDR) | 1,500 – 2,500 kg | 12 – 25 m/min | Q235B / Q355B Steel | PLC / Photoelectric Sensors | Main Inbound/Outbound Arteries & Cross-Docking |
| Double / Triple Strand Chain Conveyor | 2,000 – 3,000 kg | 10 – 18 m/min | High-Strength Alloy Chain / Steel Frame | Frequency Inverter (VFD) | Heavy Bottom Pallet Handling & Transverse Transfer |
| 2-Way Radio Shuttle Racking System | 1,000 – 1,500 kg | 35 – 50 m/min (Unloaded: 60) | Cold-Rolled Profile Steel (FEM 10.2.02) | RF Remote / WMS Auto-Sync | Deep-Lane High-Density Storage & Cold Rooms |
| 4-Way Automated Pallet Shuttle System | 1,200 – 2,000 kg | 60 – 90 m/min | High-Precision Profile Rail Steel | 5G / Wi-Fi Mesh WCS Control | Matrix Automated Storage & High-Throughput Fulfillment |
| ASRS Stacker Crane & Shuttle Hybrid | 2,500+ kg | 120 – 240 m/min (Crane) | Structural Column Heavy Profile | Fully Automated SCADA / WMS | High-Bay Clad Building Automated Warehouses |
Engineering Information Gain Insight: Structural Deflection Standards
Unlike light-duty case conveyors, pallet conveyor storage systems must be calculated to prevent structural deflection under static and dynamic loading. Top China manufacturers adhere strictly to international standards such as FEM 10.2.02 and ANSI/MH16.1 (RMI). For a standard 2,500 kg pallet payload over a 1,400 mm beam span, the structural deflection limit must not exceed L/200 (maximum 7.0 mm deflection). Excess deflection induces severe mechanical friction on roller bearings and causes positioning errors for automated stacker cranes and radio shuttles.
Future Procurement Trends for Global B2B Buyers (2025–2030)
Navigating the shift toward modularity, energy efficiency, autonomous material handling, and resilient supply chain infrastructure.
1. Modular Plug-and-Play Architecture
Global procurement teams are moving away from rigid, custom-welded single-purpose conveyor tracks. Future pallet conveyor systems utilize pre-wired, standardized modular frames with integrated bus communication (IO-Link / AS-Interface). This enables rapid onsite commissioning, dynamic expansion, and minimal downtime during layout reconfigurations.
2. AMR & AGV Interface Convergence
Modern pallet storage facilities no longer rely solely on fixed conveyors. Industrial procurement now demands seamless mechanical and digital handshakes between motorized conveyor beds, radio shuttle racks, and Autonomous Mobile Robots (AMRs). Standardized optical and wireless docking interfaces allow AMRs to drop off pallets directly onto conveyor feed lines without human intervention.
3. ESG & Low-Energy Motorization
Energy consumption in 24/7 logistics centers is a major operational expenditure. High-efficiency 24V/48V Brushless DC (BLDC) motorized drive rollers (MDR) combined with smart "run-on-demand" zone control reduce energy consumption by up to 60% compared to legacy continuous-drive AC motor networks.
4. Cold Chain & Sub-Zero Reliability
With the surge in global frozen food and pharmaceutical distribution, automated pallet shuttle racking and conveyor systems engineered for extreme temperature zones (-25°C to -30°C) represent one of the fastest-growing procurement segments. Systems require special lithium-titanate batteries, low-temperature lubricants, and stainless/galvanized structural steel finishes.
5. Total Cost of Ownership (TCO) Prioritization
Discerning procurement officers look beyond the initial FOB purchase price. They evaluate total wear-and-tear costs, availability of replacement bearings and rollers, structural warranty periods (such as Remprack's 10-year structural warranty), and local maintenance accessibility when choosing a vendor in China.
Technological Evolution: From Static Racks to Intelligent Storage Matrices
How Chinese racking manufacturers integrated mechanical engineering, robotics, and cloud telemetry into high-density storage solutions.
Phase 1: Selective Static Pallet Racking
Initial warehouse storage relied on basic teardrop or selective beam racking. While offering 100% pallet selectivity, building cube utilization remained extremely low (under 40%), requiring wide forklift operational aisles (3.5m to 4.5m).
Phase 2: High-Density Mechanical Systems
To overcome space constraints, engineers introduced Drive-In, Push-Back, and Pallet Flow Racking. These systems dramatically improved floor space efficiency but introduced operational friction, high forklift collision risks, and rigid LIFO/FIFO stock rotation limits.
Phase 3: Radio Shuttle & Conveyor Integration
The introduction of battery-powered radio shuttles running on specialized rack rails revolutionized high-density storage. By separating forklift movement from internal lane travel, throughput doubled, racking damage plummeted, and safety improved exponentially.
Phase 4 (Current State): 4-Way Autonomous Shuttles & IoT Digital Twins
Today's state-of-the-art Chinese manufacturers produce 4-Way Pallet Shuttles that navigate both longitudinal and transverse racking channels. Integrated with real-time 3D Digital Twin WCS dashboards, these systems dynamically route pallets across multiple storage levels via vertical lifts, automatically balancing warehouse workloads and predicting mechanical maintenance needs before failures occur.
Why Partner with Remprack Storage Solutions (EBILTECH)?
Two decades of OEM/ODM industrial racking leadership, rigorous quality control, and worldwide project deployment.
20+ Years Factory Manufacturing
Established in 2006 in Nanjing, China, our 40,000 square meter production facility houses continuous automatic cold-roll forming lines, robotic welding stations, and automated electrostatic powder coating systems capable of delivering high structural precision.
Triple Certified Compliance
All products strictly adhere to international engineering standards. We hold active certifications for CE (Europe), ISO 9001 (Quality Management), ISO 14001 (Environmental), and TUV Rheinland structural safety audit approvals.
10-Year Comprehensive Warranty
We stand behind our steel structural integrity and conveyor fabrication. Every installed system compliant with our operational load limits is backed by an industry-leading 10-year structural warranty and lifetime technical engineering support.
Worldwide Project Deployment
Exporting to more than 85 countries across North America, South America, Europe, Southeast Asia, the Middle East, and Africa. We provide complete export packaging, CAD/3D system drawings, and optional overseas installation engineering assistance.
Custom Engineering & OEM/ODM
Our in-house R&D engineering team custom-designs racking profiles, beam connectors, roller spacing, chain specs, powder-coat RAL colors, and branded OEM labels to match distributor catalog specifications and project requirements.
Frequently Asked Questions (FAQ) for Pallet Storage Sourcing
Expert engineering answers to critical questions regarding design, load capacity, lead times, and system compatibility.
What precise technical parameters are required to calculate a pallet conveyor or shuttle system quote?
1. Warehouse Architectural Layout: CAD or PDF drawing showing clear height under building trusses/sprinklers, floor slab thickness, and column locations.
2. Pallet Specifications: Width x Depth x Height, bottom board orientation (2-way vs. 4-way entry), and maximum/minimum unit load weight (including pallet).
3. Forklift / AMR Specs: Lift height capacity, turning radius, and fork dimensions.
4. Throughput Rate: Target pallets handled per hour for inbound receiving, storage transfer, and outbound dispatch zones.
5. Environmental Parameters: Operating ambient temperature (room temp, chilled, or -30°C cold room) and local seismic code requirements.
How do I determine whether to choose a Radio Shuttle System or a Pallet Conveyor System?
What steel grades and surface treatment processes are used for export orders?
What is the standard manufacturing lead time and export container packing method?
How are installation and maintenance handled for international project deployments?
Optimize Your Warehouse Density & Conveyor Throughput Today
Connect directly with our senior application engineers in Nanjing, China. We will analyze your floorplan CAD and provide a customized layout proposal, load calculations, and competitive direct-factory pricing within 24 hours.