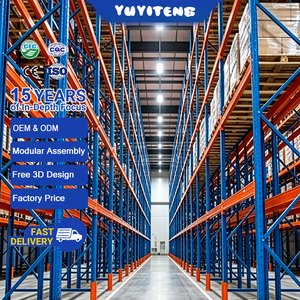
Heavy-Duty Drive-In & High-Density Racking Systems
Direct-from-factory custom OEM/ODM racking engineered to maximize volumetric storage efficiency by up to 85%.
12 Layer Steel Automated Storage System Drive-In Pallet Rack Warehouse Retrieval Shelving Powder Coated 2.5-6m
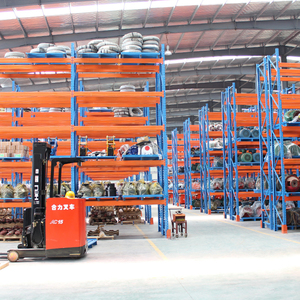
Best Selling Customized Warehouse Drive in Rack Steel Pallet Racking System Heavy Duty Industrial Warehouse Steel Rack
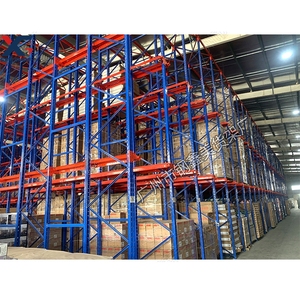
Boltless Metal Steel Stacked Parking System Refrigerated Warehouse Drive-in Rack Double Pallet Rack System
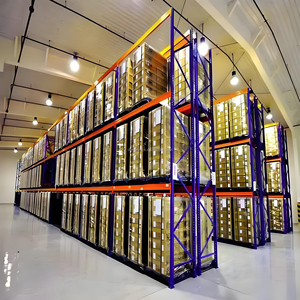
Space Saving Warehouse Storage Solution Forklift Entry System High Density Drive in Rack
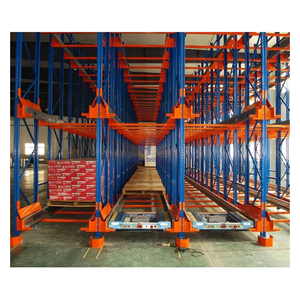
Customized Used High Quality Steel Heavy Duty Automatic Storage System Shuttle Pallet Rack For Warehouse

OEM High-Tech Radio Shuttle Pallet Rack Industrial Steel Automatic Warehouse Racking System For Storage
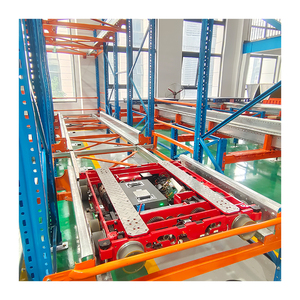
Car Shuttle Rack 4 Direction Pallet Mobile Rack System Warehouse Storage Equipment Four-Way Radio Shuttle Racking With Efficient
85%
Space Utilization Rate
2006
Established Manufacturing Year
85+
Global Export Markets
10-Yr
Structural Structural Warranty
Engineering Architecture of High-Density Drive-In Pallet Racking
In modern industrial logistics and cold-chain supply chains, real estate overhead represents one of the largest capital expenditures. Standard selective pallet racking systems dedicate up to 60% of total warehouse floor area to forklift operational aisles. **Drive-In Pallet Racking Systems**, engineered by premier Chinese manufacturers like Remprack Storage Solutions, eliminate conventional access aisles by allowing counterbalanced or reach forklifts to drive directly into the racking lanes. This structural design enables dense block-storage of homogeneous SKUs, delivering volumetric footprint gains of up to 85% compared to conventional storage profiles.
Drive-in racking operates primarily on a **Last-In, First-Out (LIFO)** inventory control methodology. For facilities requiring First-In, First-Out (FIFO) rotation, **Drive-Through Racking** configurations are deployed, incorporating dedicated entry faces on one side and exit faces on the opposite side. Understanding the mechanical structural loads, metallurgy, dynamic load distribution, and safety parameters is vital for supply chain directors seeking to optimize warehouse density.
Structural Component Metallurgy & Engineering Dynamics
Unlike standard pallet racking where beams span horizontally between upright frames to support pallets directly, drive-in systems utilize continuous **cantilever support arms** welded or bolted to vertical cold-rolled steel upright profiles. Pallets rest on heavy-duty continuous support rails running the entire depth of the bay lane.
High-Yield Q235B / Q355B Steel
Manufactured using high-tensile cold-rolled structural steel compliant with ISO 9001 and CE norms, ensuring high yield strength under heavy static and dynamic impact forces.
Heavy-Duty Cantilever Arms
Tapered arm geometry engineered to maximize vertical clearance while maintaining high moment-resistance against eccentric loading and driver impact.
Floor Guide Rail Systems
Extruded steel floor channels guide forklift trucks safely down deep storage lanes, preventing upright frame strikes and accelerating cycle times.
Technical Specification Matrix: Drive-In vs. Alternative High-Density Racking
| Racking Architecture | Storage Density | Pallet Selectivity | Inventory Rotation | Cost Per Pallet Position | Optimal SKU Profile |
|---|---|---|---|---|---|
| Drive-In Racking | Very High (80-85%) | Low (1 SKU per lane) | LIFO | Low to Moderate | High-volume, low-SKU count, seasonal or cold storage |
| Selective Pallet Racking | Low (35-40%) | 100% Immediate | FIFO / LIFO | Lowest Initial CapEx | High SKU variance, fast-moving consumer goods (FMCG) |
| Radio Shuttle Racking | Maximum (85-90%) | Moderate (Per lane) | FIFO or LIFO | Moderate to High | Cold storage, high throughput, automated integration |
| Push-Back Racking | High (65-75%) | Moderate (2-6 deep) | LIFO | Moderate | Medium SKU volume, faster loading cycle times |
| VNA (Very Narrow Aisle) | High (60-70%) | 100% Immediate | FIFO | Moderate | High-bay warehouses with specialized VNA trucks |
Why Sourcing Drive-In Racking from Remprack Storage Solutions Offers Superior Competitive ROI
Founded in 2006 in Nanjing, China, Remprack Storage Solutions Co., Ltd. has established itself as an authoritative global leader in the design, engineering, and manufacturing of heavy-duty industrial storage racks. Spanning over 40,000 m² of modern production facilities equipped with automated CNC roll-forming lines, robotic welding workcells, and automated electrostatic powder coating lines, Remprack delivers unmatched structural safety and precision manufacturing.
Engineered in compliance with European EN 15512 structural design codes, FEM standards, and American RMI specifications, Remprack drive-in racking systems have been exported to over 85 countries across Europe, the Americas, Asia-Pacific, the Middle East, and Africa.
Certified Quality Compliance
Fully certified under CE, ISO 9001 (Quality Assurance), ISO 14001 (Environmental Management), and TUV Rheinland safety standards for rigorous international engineering acceptance.
Tailored OEM & ODM Capability
From custom upright pitch configurations and specialized structural steel gauges to proprietary powder-coat colors and custom anti-corrosion galvanizing for severe environments.
10-Year Comprehensive Structural Warranty
Every system undergoes Finite Element Analysis (FEA) load simulation and carries a 10-year factory warranty when operated under standard load parameters.
Advanced Cold Storage Application & Thermal Efficiency Optimization
Cold storage facilities operate under intensive electrical expense, where every cubic meter of refrigerated space carries significant operational overhead. Drive-in pallet racking systems engineered by China manufacturers provide maximum thermal efficiency by eliminating air gaps caused by redundant aisles. By packing pallets in a tight block grid, cold air distribution is concentrated through designated flue spaces, reducing energy consumption per pallet position by up to 35% in sub-zero environments (-25°C to -30°C).
Future Procurement Trends & Technological Evolution in Industrial Storage
As global logistics shifts toward smart warehousing, automation, and ESG compliance, the drive-in pallet racking sector is evolving rapidly. Procurement managers and supply chain directors must account for several emerging trends when specifying storage equipment from China manufacturers:
1. Hybrid Shuttle Integration (Drive-In to Radio Shuttle Upgrades)
Traditional drive-in racking relies on forklift drivers operating inside narrow upright channels, which introduces potential frame collision risks and limits travel speed. Modern enterprise facilities are increasingly procuring **Shuttle-Ready Drive-In Structures**. These structural frames accept semi-automated or fully automated radio shuttles running along the depth rails. This hybrid transformation eliminates forklift entry entirely, increasing throughput speeds by 40% while preserving the high spatial density of traditional drive-in layouts.
2. Seismic-Resistant & Finite Element Analyzed (FEA) Structural Geometries
Global logistics hubs situated in high-seismic zones (such as South America, Southeast Asia, and the Pacific Rim) require advanced dynamic load calculations. Leading Chinese racking suppliers utilize 3D FEA stress-strain modeling to design specialized top-tie beam networks, back bracing diagonals, and floor anchor assemblies capable of absorbing kinetic energy during seismic movements without structural buckling.
3. Green Steel Traceability & Low-Carbon Surface Coatings
International buyers subject to Carbon Border Adjustment Mechanisms (CBAM) and strict Scope 3 emission targets demand sustainable supply chains. Premier manufacturers are adopting fully traceable hot-rolled coil steel sourced from low-emission steel mills, coupled with zero-VOC, heavy-metal-free thermosetting powder coatings that emit no volatile organic compounds during curing.
4. IoT-Enabled Structural Health & Collision Monitoring
To reduce workplace safety hazards, next-generation drive-in racking installations incorporate wireless strain gauges, ultrasonic collision detection sensors, and tilt indicators mounted to critical upright bases. These IoT sensors communicate directly with Warehouse Management Systems (WMS), alerting facility maintenance teams to structural impacts or eccentric load deflections in real time.
Request an Engineered Layout & Structural Quotation
Send your warehouse CAD layout, pallet metrics, and load requirements to our senior engineering team for a complimentary high-density optimization plan.
Inquire NowFrequently Asked Questions (FAQ) - Drive-In Pallet Racking Sourcing
Key technical and procurement inquiries addressed by our engineering team to assist global buyers in system selection and structural safety planning.
What warehouse parameters are required to calculate a custom Drive-In Racking proposal?
To prepare an accurate engineering proposal and CAD layout, our structural design team requires:
- Warehouse floor plan layout (CAD dwg format or detailed PDF) with building column grid locations.
- Clear height under building trusses, roof pitch, lighting, or fire sprinkler systems.
- Exact pallet dimensions (Width x Depth x Height including cargo overhang).
- Maximum and average pallet weight loads (kg per pallet position).
- Forklift truck model specifications, overall width, mast collapse height, and maximum lift height.
- Operating environment temperature ranges (e.g., ambient warehouse vs. -25°C cold storage).
How does Drive-In Racking manage structural safety and prevent forklift impacts?
Because forklifts operate inside the racking structure, safety engineering is paramount. Remprack integrates multi-stage protective systems: ground-mounted heavy-duty steel guide rails (floor channels) to keep forklifts centered; heavy-gage column protectors at the entry aisle uprights; tapered entry brackets on pallet support rails; and bright safety-yellow powder coat finishes for high visibility inside deep lanes.
What is the maximum recommended depth for a Drive-In racking lane?
While lanes can theoretically be built up to 10 or more pallets deep, standard industry practice recommends 4 to 8 pallets deep per lane for optimal operational efficiency. Deep lanes exceeding 8 pallets can slow forklift maneuvering times and increase driver fatigue unless floor guide rails or radio shuttle automation are incorporated.
What international structural engineering standards do Remprack systems comply with?
Our drive-in pallet racking systems are engineered strictly in accordance with European FEM 10.2.07 and EN 15512 structural steel design codes, American RMI (Rack Manufacturers Institute) standards, and Australian AS4084 standards. All load ratings are verified via Finite Element Analysis (FEA) and physical coupon testing.
Can standard wooden or plastic pallets be used in Drive-In Racking?
Yes, standard Euro-pallets (800x1200mm), GMA pallets (48x40 inch), industrial wooden pallets, and steel/plastic pallets can be accommodated. However, because pallets rest on continuous side rails rather than full horizontal beams, pallets must possess sufficient bottom runner strength without dynamic center deflection. High-density polyethylene (HDPE) or reinforced steel pallets are recommended for exceptionally heavy loads.
What is the typical manufacturing lead time for container orders from China?
Standard factory manufacturing lead time for standard 40ft high-cube container orders (approx. 20-25 metric tons of finished structural steel racking) is 14 to 21 days from order confirmation and drawing approval. Custom colors, hot-dip galvanizing, or specialized OEM roll-forming profiles may require 25 to 30 days.
What warranty protection is provided for international procurement projects?
Remprack provides a 10-year limited structural warranty covering material defects, structural steel failure, and weld integrity under normal specified loading conditions. Complete installation manuals, assembly elevation drawings, load capacity placards, and remote video technical support are provided with every export shipment.
How do I choose between a traditional Drive-In system and a Radio Shuttle system?
Traditional Drive-In systems offer lower upfront capital expenditure (CapEx) per pallet position and are ideal for operations with moderate turnover rates and budget constraints. Radio Shuttle systems carry higher initial costs due to automated shuttle units, but provide significantly faster cycle times, higher safety margins, support both FIFO and LIFO rotation, and minimize forklift maintenance costs over a 5-to-10-year lifecycle.
Partner with China's Premier Racking Manufacturer Today
Optimize your warehouse cubic capacity, lower operational costs, and secure high-grade industrial rack systems backed by CE, ISO 9001, and TUV certifications.
Inquire Now