High-Performance Storage & Automated Warehousing Systems
Explore our export-grade industrial racking catalog. Engineered to CE, ISO 9001, and TUV international structural standards for heavy-duty logisitics optimization.
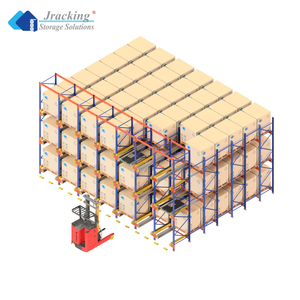
Jracking Automatic Warehouse System Factory Direct Sale High Intelligent Automated Pallet Runner Four Way Radio Shuttle Rack
Ultra-high density intelligent shuttle solution optimized for multi-directional autonomous pallet movement in cold chain and logistics hubs.
Contact Us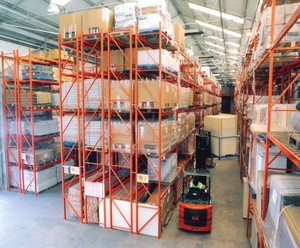
Double Deep Pallet Racking High Capacity Storage System Suitable for Reach Truck Forklift Optimize Warehouse Space Utilization
Increases storage density by 30-40% compared to standard selective racking using specialized pantograph reach trucks.
Contact Us
SHUNLI Cold Rolled Steel 5 Layer Heavy Duty Industrial Warehouse Storage Anti-corrosion Adjustable Bolt Free Powder Coated Shelf
Versatile heavy-duty shelving modules manufactured from premium Q235B steel with electrostatic anti-corrosion coating.
Contact Us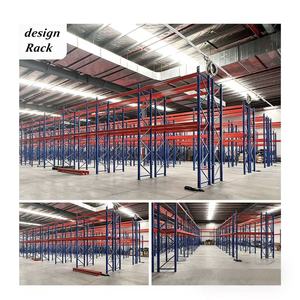
Certificated Bolted Heavy Duty Industrial Forklift Stacking Rack Selective Shelves Storage Rack Pallet Racking
100% selective pallet access engineered for high throughput distribution centers requiring flexible shelf height adjustments.
Contact Us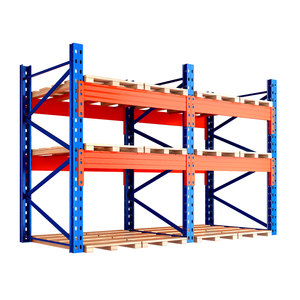
Heavy Duty Industrial Storage Shelves System Metal Rack Stacking Units Warehouse Steel Industrial Pallet Racking
Modular industrial structural frame configurations capable of bearing unit loads exceeding 4,000 kg per level.
Contact Us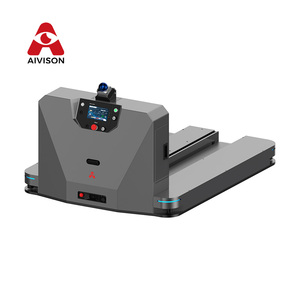
China AGV Manufacturer Automated AMR Open Pallet /Closed Pallet Handling Robot For Warehouse Logistics
Next-generation laser-guided Autonomous Mobile Robots (AMR) designed for seamless integration with multi-tier mezzanine floors.
Contact Us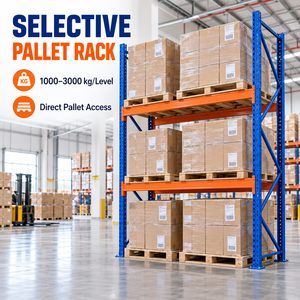
Heavy Duty Selective Pallet Rack Industrial Warehouse Storage Racking System for Pallet Storage
Standard industrial workhorse storage framework engineered for safety, structural rigidity, and seamless expansion.
Contact Us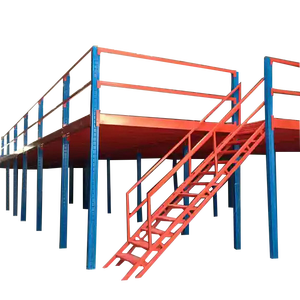
Customized Heavy Load Mezzanine Floor Rack Warehouse Shelf Racking System 2 Layers Corrosion Protection ISO9001/CE Steel Steel
Integrated multi-level rack supported mezzanine platform engineered to maximize overhead vertical cube utilization.
Contact UsEngineering Architecture of CE Certified Rack Supported Mezzanine Systems
In modern industrial logistics and high-density fulfillment hubs, spatial efficiency directly dictates operational profitability. A Rack Supported Mezzanine System represents the pinnacle of vertical space optimization, effectively doubling or tripling usable warehouse square footage without the exorbitant capital expenditure of facility expansion or structural building modifications. Unlike traditional structural steel platform mezzanines that rely exclusively on heavy I-beams and wide-flange columns, rack-supported platforms utilize the heavy-duty pallet racking frames themselves as the primary load-bearing substructure.
As an established OEM/ODM manufacturer certified under strict CE (Conformité Européenne), ISO 9001, ISO 14001, and TUV criteria, our structural design philosophy integrates rigorous finite element analysis (FEA) compliant with EN 15512 (European Standard for Steel Static Storage Systems) and FEM 10.2.02 standards. This structural guarantee ensures complete seismic safety, resistance to structural buckling, and maximum operational longevity under continuous multi-shift usage.
Cold-Rolled Upright Profiles
Manufactured from premium Q235B and Q355B high-tensile steel coils. Our cold-rolled uprights feature multi-bend diamond or teardrop punch patterns engineered to withstand severe axial compressive forces while minimizing torsional deflection.
Interlocking Floor Decking Options
Engineered deck surfaces tailored to operational workflow: heavy-duty perforated steel grating for sprinkler water penetration, solid chequered anti-slip steel plates, or high-density structural MDF overlay boards backed by steel deck channels.
Safety Infrastructure & Access Controls
Integrated full-height perimeter handrail systems, toe-boards, kick-plates, dual-action safety pallet gates (up-and-over or sliding), and custom-pitched structural staircases compliant with global OSHA and EU safety directives.
Technical Specification & Decking Selection Matrix
Selecting the optimal structural configuration depends on localized weight requirements, material handling equipment (MHE) usage, fire prevention compliance, and light reflection priorities. Review our technical performance matrix below:
| Decking Type | Standard Load Capacity | Surface Properties | Fire & Sprinkler Compliance | Best Industry Application |
|---|---|---|---|---|
| Perforated Steel Grating | 500 - 1,200 kg / m² | High light transmission, anti-slip grid | 100% Water Penetration (NFPA Compliant) | Chemical, Hazardous Goods, Cold Storage |
| Chequered Steel Plate | 300 - 1,500 kg / m² | Heavy-duty impact resistant, anti-skid pattern | Solid Barrier (Requires lower level sprinklers) | Heavy Machinery, Automotive, Heavy Spare Parts |
| B-Decking with Wood Finish | 300 - 800 kg / m² | Smooth foot traffic, noise damping | Combustible / Standard Fire Protection | E-Commerce Picking, Garment & Textile Storage |
| Galvanized Steel Planks | 400 - 1,000 kg / m² | Corrosion resistant, seamless interlocking | Slotted options available (up to 50% flow) | Pharmaceuticals, FMCG, Cleanroom Logistics |
Future Procurement Trends in Rack Supported Mezzanines (2026–2030)
As global supply chains transition toward hyper-automation and rapid order fulfillment, the structural specifications of rack-supported mezzanines are undergoing a technological evolution. Modern procurement officers and facility planners must account for key emerging trends:
- Autonomous Mobile Robot (AMR) & AGV Floor Integration: Modern mezzanine decks are increasingly engineered with precise floor flatness tolerances (super-flat floors) and anti-static coatings to accommodate high-speed sorting AMRs operating on elevated platforms.
- Hybrid Automated Storage and Retrieval Systems (ASRS): Rack-supported mezzanines are now being designed with modular cutouts and structural reinforcement to integrate overhead crane tracks, vertical reciprocating conveyors (VRCs), and 4-way radio shuttles.
- Sustainable Powder Coating & Eco-Steel Sourcing: Environmental, Social, and Governance (ESG) mandates require suppliers to utilize non-VOC electrostatic powder coatings and certified zero-carbon recycled steel billets without compromising tensile yield strength.
- Modular "Plug-and-Play" Structural Scalability: Modern B2B buyers favor demountable, bolt-together beam-to-column locking systems over permanently welded structures, enabling seamless relocation or height expansion as inventory demand fluctuates.
Enterprise Manufacturing & Global OEM/ODM Dominance
Over two decades of precision engineering, continuous metallurgical R&D, and export excellence serving logistics leaders across 85+ countries.
CE & International Certifications
Our complete production line operates strictly under ISO 9001 quality management and ISO 14001 environmental frameworks. All rack-supported mezzanine components bear valid CE marks and TUV structural safety verification.
Custom CAD / 3D BIM Structural Design
We provide full engineering support before contract signing. Our in-house structural engineers generate precise 2D CAD layouts, 3D Building Information Modeling (BIM) structural files, and seismic stress analysis reports tailored to your floor plan.
Advanced Automated Production Base
Spanning over 40,000 square meters, our facility houses continuous automatic cold roll-forming lines, robotic welding stations, and automated Swiss-Gema electrostatic powder coating lines to guarantee sub-millimeter manufacturing precision.
Frequently Asked Questions on Mezzanine Procurement
Essential technical, financial, and logistical insights for project managers, warehouse engineers, and procurement directors.
To deliver an optimized structural proposal, our engineering team requires: (1) Architectural warehouse CAD drawings showing column grid spacing and clear height under sprinklers or joists; (2) Concrete slab thickness and compressive strength rating (e.g., C25/C30); (3) Pallet sizes, unit loads, and desired weight capacity per deck level (kg/m²); and (4) Preferred material handling access methods (forklift, VRC hoist, or staircases).
Rack-supported mezzanines are generally 25% to 45% more cost-effective per square meter than structural I-beam platforms. Because the underlying pallet rack components serve a dual role—providing high-density rack storage below while supporting the floor above—material efficiency is maximized and total steel weight is optimized without sacrificing structural stability.
Our rack-supported mezzanine systems are engineered in strict accordance with European standards EN 15512 and FEM 10.2.02, as well as American RMI (Racking Manufacturers Institute) regulations. All components carry CE compliance certificates, and our factory operates under ISO 9001 and ISO 14001 quality systems. Certificates and third-party TUV test reports are supplied with project documentation.
For operations involving heavy hand pallet trucks or electric stackers, we recommend heavy-duty chequered steel floor plates or high-density galvanized steel planks supported by concentrated sub-floor stiffeners. If fire regulations require sprinkler water penetration to lower levels, heavy-duty open steel grating is the optimal solution.
We provide a comprehensive 10-Year Structural Product Warranty across all cold-rolled steel racking frames and floor supports. For international projects, we supply detailed 3D step-by-step installation drawings, component identification labeling, container loading optimization, and optional on-site or remote engineering guidance.
Ready to Optimize Your Vertical Storage Cube?
Partner directly with China’s premier CE-certified rack-supported mezzanine manufacturer. Request a complimentary structural layout engineering consultation and factory-direct quote today.