Application

Custom structural engineering solutions designed for high-density logistics, heavy manufacturing, cold storage, FMCG, and chemical warehousing worldwide.

Tailored Storage Systems

High-Performance Racking Solutions by Industry Sector

With over two decades of experience since 2006, Remprack Storage Solutions Co., Ltd. delivers certified, load-tested warehouse racking systems optimized for international safety standards, seismic compliance, and maximum spatial utilization.

Logistics & 3PL

High pallet rotation speed, multi-SKU flexibility, and fast order pick times.

Manufacturing

Heavy load capacity, raw material buffers, and long bar stock cantilever systems.

Food & Beverage

Strict FIFO compliance, zero-contamination steel surfaces, and gravity flow channels.

Cold Chain

Maximum volume utilization down to -30°C with automated shuttle & mobile racks.

Heavy duty logistics racking system manufactured by Remprack Storage Solutions Co., Ltd.

Logistics & 3PL Distribution Warehousing

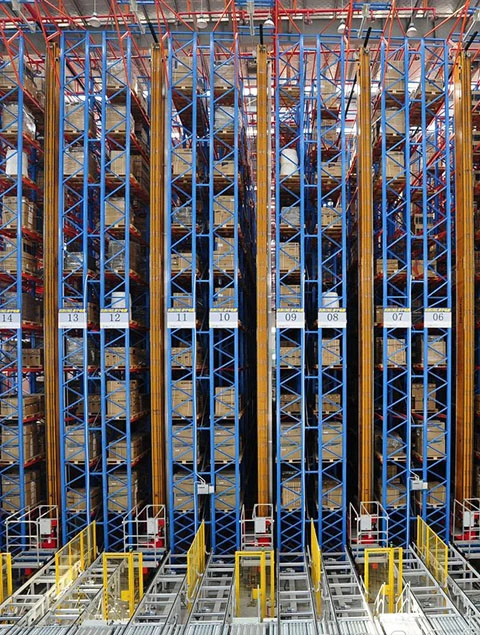
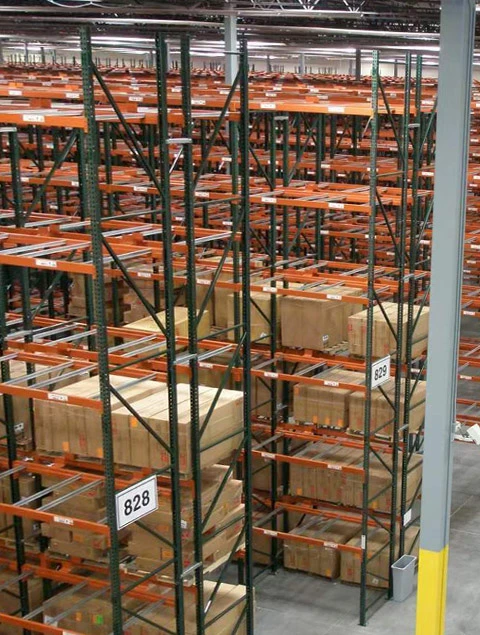
Modern third-party logistics centers require scalable storage architecture capable of handling thousands of mixed SKUs with high daily throughput. Remprack Storage Solutions Co., Ltd. designs heavy-duty selective pallet racking, Very Narrow Aisle (VNA) systems, and multi-tier picking structures that maximize vertical clear height while offering 100% immediate pallet accessibility.

Recommended Racks: Selective, VNA, Radio Shuttle
Load Capacity: 1,000 kg - 4,500 kg per level
Key Advantage: 100% SKU selectivity & high pick rates
Compliance: CE, ISO 9001, FEM 10.2.02 Standards

All structural uprights utilize high-tensile Q355B steel profiles roll-formed in-house, ensuring robust resistance to forklift impact and long operational life.
Industrial Manufacturing & Assembly Plants

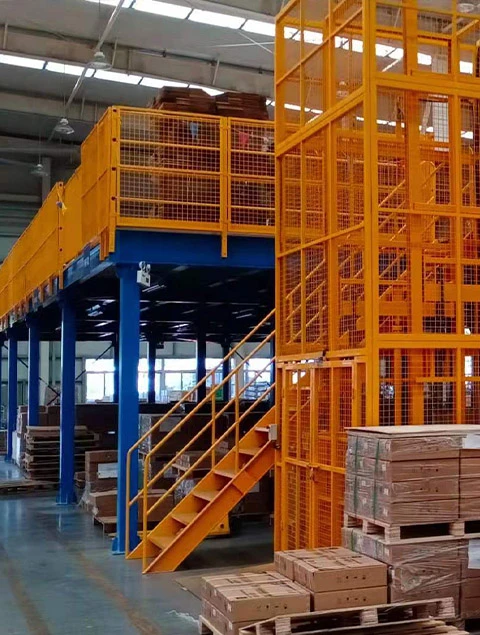
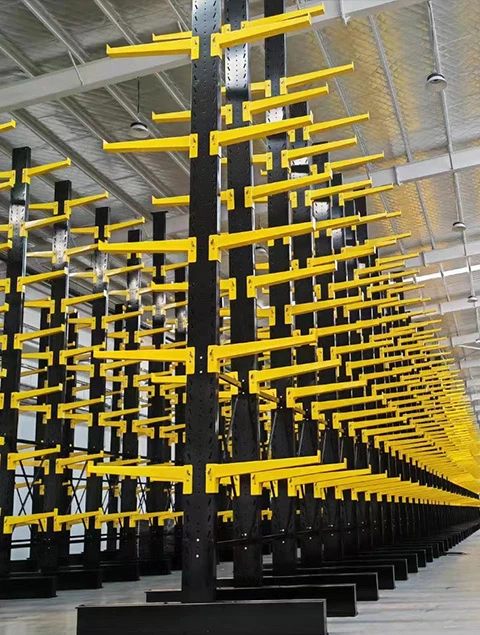
Manufacturing supply chains demand specialized racking for heavy raw materials, work-in-progress (WIP) inventories, tooling dies, and non-standard long components. Our custom heavy-duty cantilever racks and structural steel mezzanine floors turn overhead airspace into productive storage or office floors, preventing factory floor clutter and reducing material transfer times.

Recommended Racks: Cantilever, Mezzanine, Heavy Pallet
Arm/Deck Capacity: Up to 1,500 kg per cantilever arm
Key Advantage: Obstruction-free long stock storage
Surface Finish: Powder Coated / Hot-Dip Galvanized

Engineered with safety lock pins and finite element analysis (FEA) structural calculations for continuous heavy industrial duty cycle safety.

Industrial cantilever and manufacturing rack system designed by Remprack
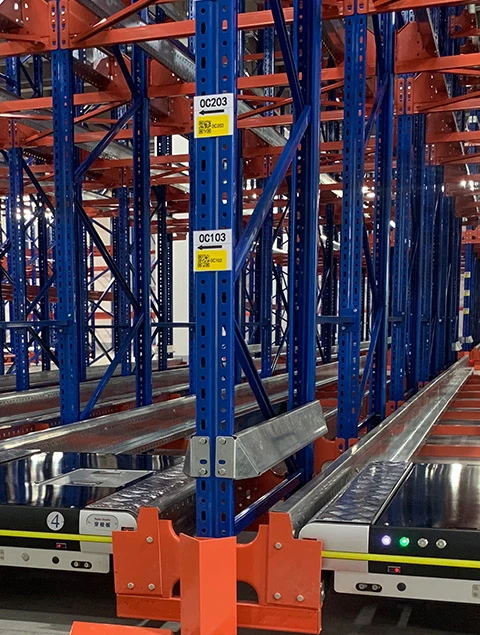
Radio shuttle high density pallet racking for food and beverage industry

Food, Beverage & FMCG Cold Logistics

Perishable food items and fast-moving consumer goods require strict batch control, rotation tracking, and hygienic storage environments. Remprack Storage Solutions Co., Ltd. provides gravity pallet flow racks for strict First-In, First-Out (FIFO) stock management, alongside semi-automated radio shuttle pallet racking systems that double floor space utilization in temperature-controlled environments.

Recommended Racks: Radio Shuttle, Pallet Flow, Drive-In
Stock Rotation: FIFO & LIFO Automated Options
Key Advantage: Reduced cold store power consumption
Hygiene Standard: Non-toxic epoxy powder coating

Optimized rail geometries minimize friction, allowing reliable shuttle transit speed inside deep lanes up to 40 meters deep.

Pharmaceutical & Healthcare Warehouses

Pharmaceutical supply chains demand spotless traceability, tight aisle management, and zero dust accumulation on stored products. Remprack Storage Solutions Co., Ltd. engineers high-density cleanroom steel racking and steel pallet systems designed to meet international Good Distribution Practice (GDP) requirements, providing maximum airflow and clear SKU label positioning.

Recommended Racks: VNA Pallet, Steel Shelving, ASRS
Material Options: Galvanized, Stainless Steel, Steel Pallets
Key Advantage: High sanitation & inventory visibility
Quality System: TUV & ISO 14001 Certified

Custom structural designs incorporate smooth anti-bacterial coatings and wire mesh decking options to facilitate fire sprinkler penetration.

Pharmaceutical warehouse racking system by Remprack Storage Solutions Co., Ltd.
Chemical warehouse heavy duty containment racking system

Chemical & Hazardous Material Facilities

Chemical drum and hazmat storage mandates strict structural stability, corrosion resistance, and containment integration. We deliver engineered push-back racking, heavy-duty drive-in systems, and customized chemical pallet racks featuring hot-dip galvanization and containment tray supports to safeguard your operations against accidental spills or harsh ambient atmospheres.

Recommended Racks: Push Back, Drive-In, Galvanized Steel
Corrosion Proofing: Hot-Dip Galvanized (HDG) ISO 1461
Key Advantage: Chemical spill resistance & seismic anchoring
Safety Testing: Third-party structural load tested

Heavy-duty baseplates and heavy floor anchor bolts guarantee stability under dynamic load shifts and localized seismic loads.

Engineering Rigor & Global Execution

Why Overseas Procurement Officers Choose Remprack

Since 2006, Remprack Storage Solutions Co., Ltd. has delivered turnkey engineering support to distributors, logistics integrators, and industrial facility owners in 85+ countries. Every racking system starts with detailed CAD layout calculations, structural finite element modeling, and full traceability from raw steel coils to export container loading.

Need a Custom Racking Layout for Your Facility?

Send us your warehouse CAD drawing, building clearance height, and pallet specifications. Our engineering department will supply a detailed CAD layout proposal and structural quote within 24 hours.